Expand Machinery and Hasegawa, the full GEN TURN and GEN MILL range.
Founded in 1985, Expand Machinery builds the GEN TURN Swiss and turn-mill lathes and the GEN MILL machining centers, and imports the Made-in-Japan models built by Hasegawa Machine Works. Everything LOMA supplies from Expand is on this page — the Japanese-built flagships, the featured PM320-5X-T, both full ranges, automation and a customer case study.
Shopping by machine type instead? Swiss lathes · Turn-mill · Gang-tooled · Vertical machining centers
 Made in Japan · Hasegawa Machine Works
Six models in the Expand lineup are built by Hasegawa Machine Works in Japan — and they are the ones to reach for when the tolerance is the whole job. Hasegawa’s credo is “the leading edge in small machines”: in-house-manufactured spindles and milling turrets, symmetrical thermally-stable construction, and a rigid horizontal bed. That is the pedigree behind the repeatability — part 1 to part 5,000, first shift to third.
Imported and supported by Expand Machinery, so Japanese build quality arrives with a North American parts room, service team, and training center behind it — and one accountable source in the Northeast. Select models are held in U.S. inventory for immediate delivery. And they automate: robot load/unload and pallet-based unattended running are proven on this platform, not a bolt-on afterthought.


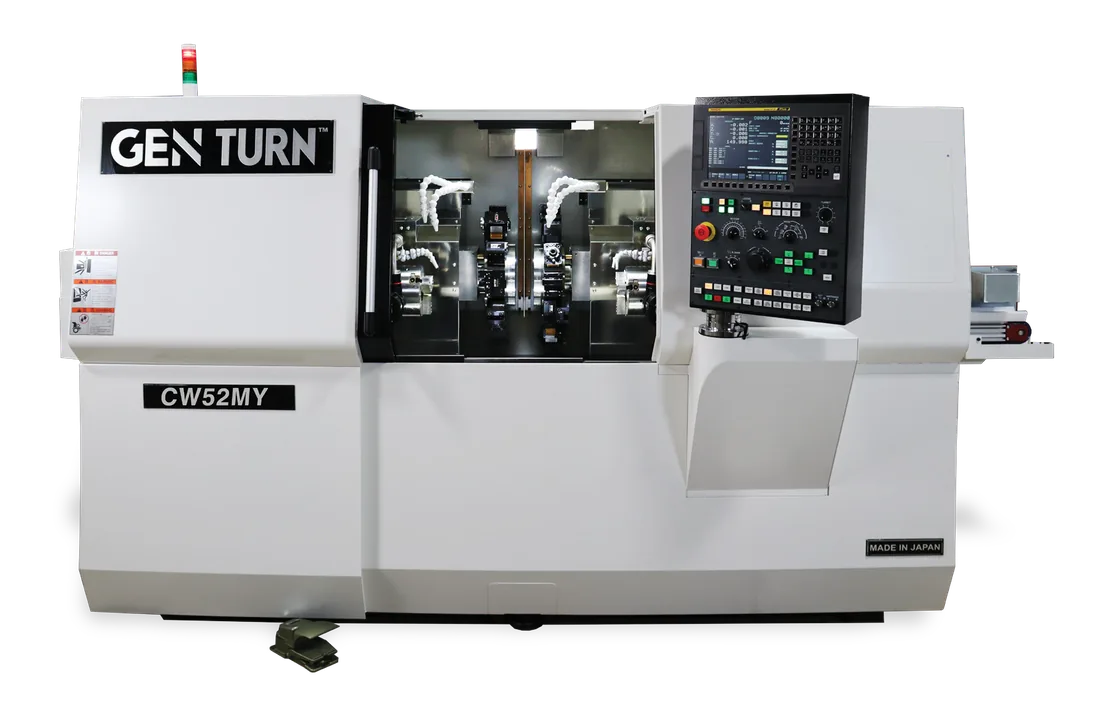
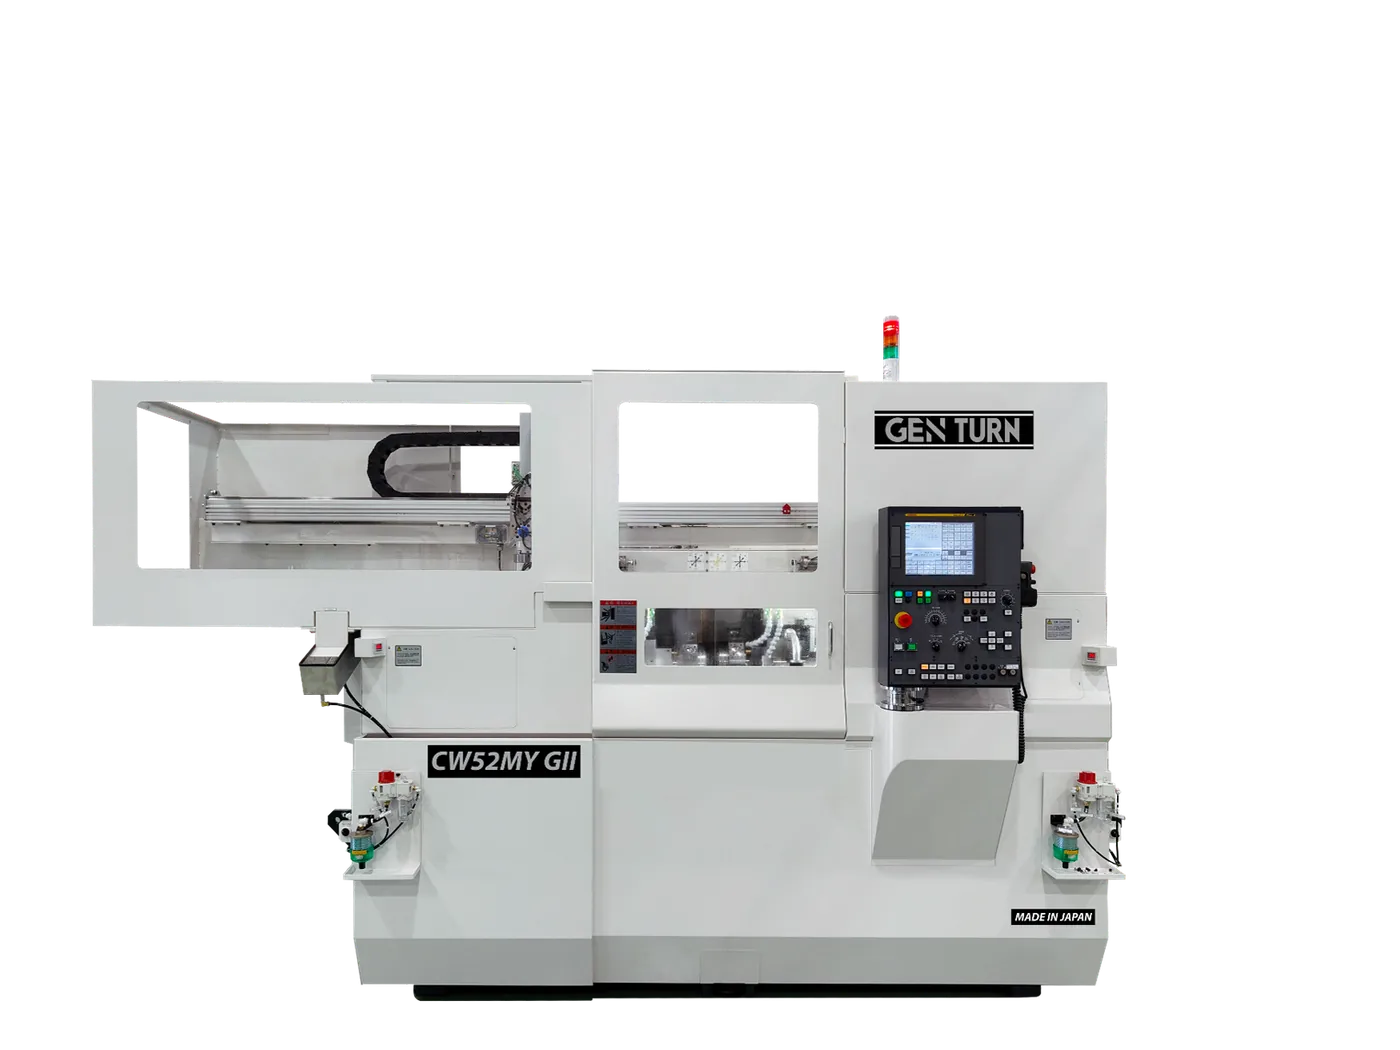
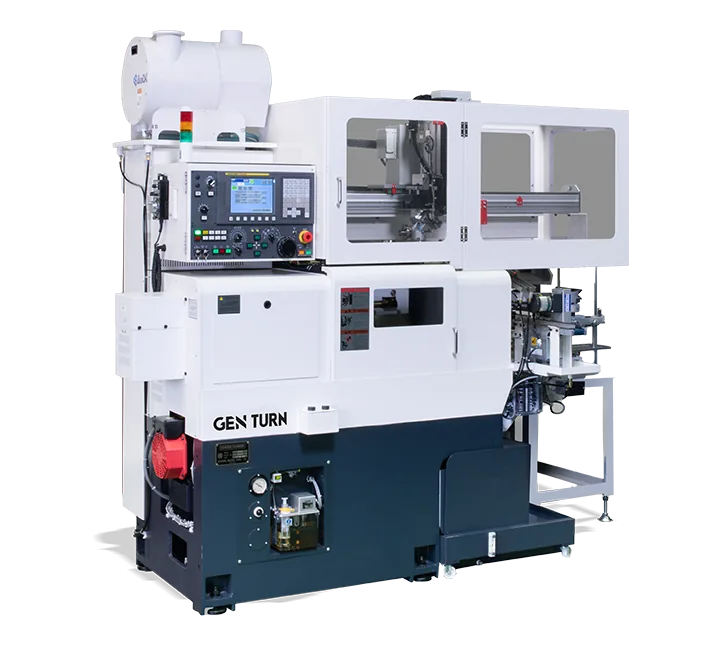
Wataru Hasegawa began building small lathes in Tokyo in 1928. While the rest of the industry chased medium and large machine tools, Hasegawa deliberately built nothing but small ones — on the conviction that high-precision work on small parts demands a machine designed around small parts. Post-war, that decision paid off when Japan’s optical industry came looking for machines that could hold watch-part tolerances. Every model in the line since has descended from that one commitment.
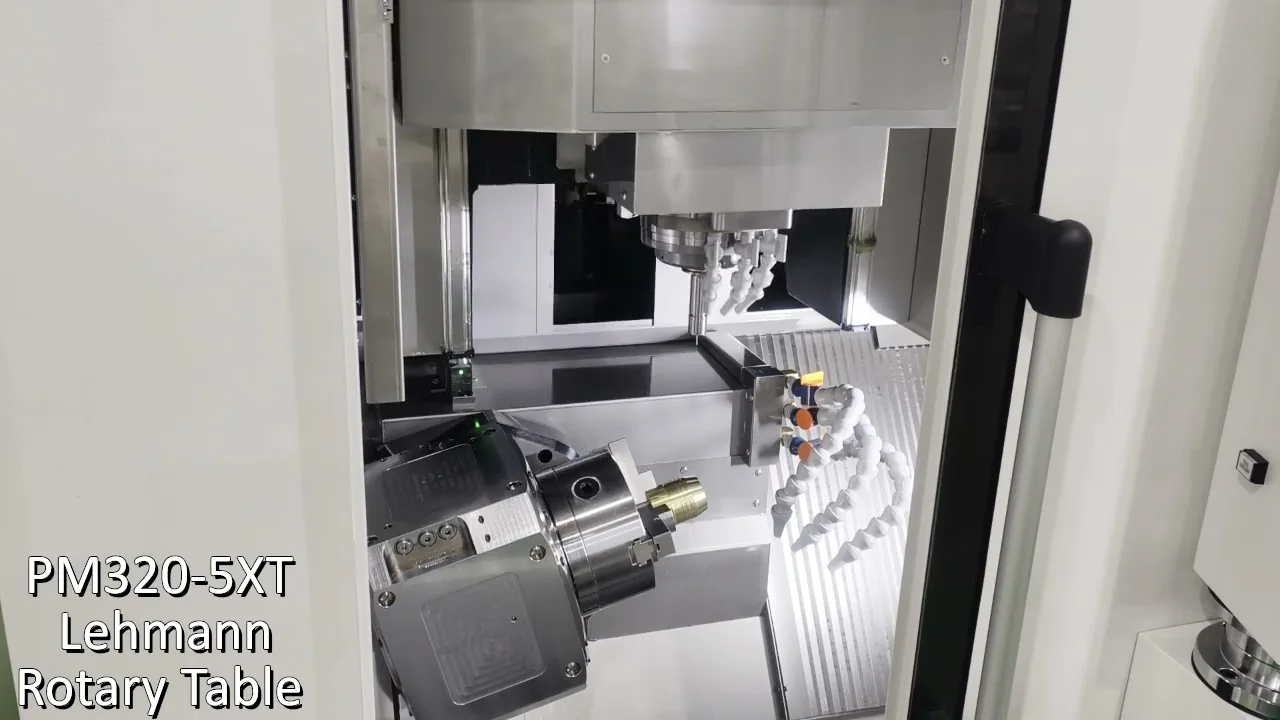
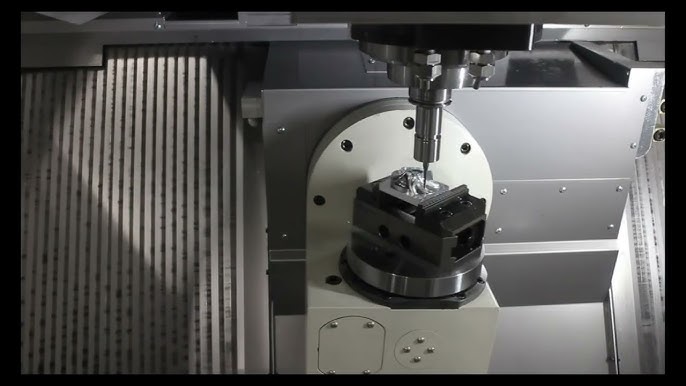

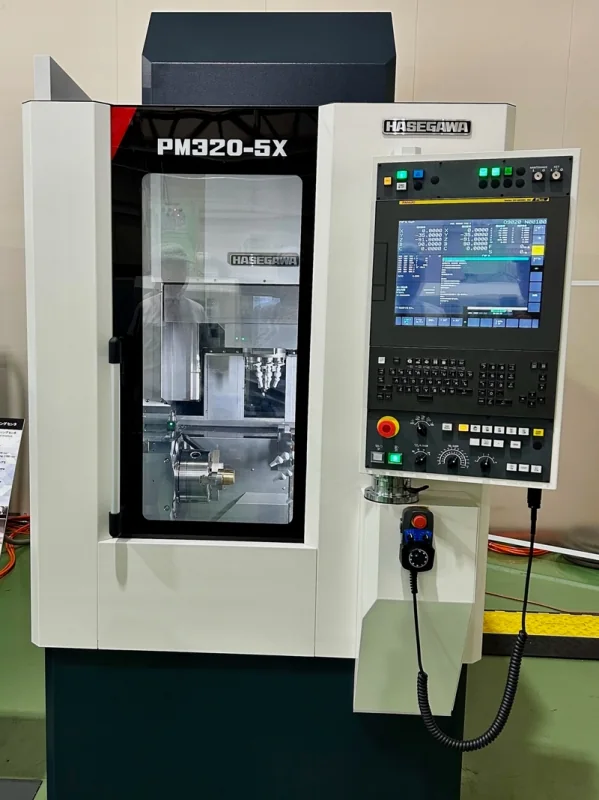
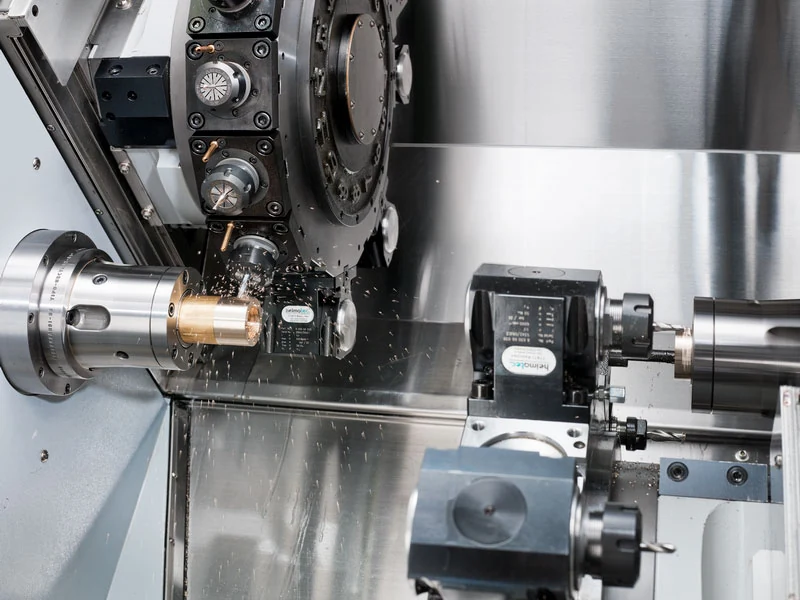
One compact machine that mills in full 5-axis and turns. The PM320-5X-T pairs a 25,000 RPM built-in spindle with a 2,000 RPM turning capability on a 150 mm trunnion table — so complex precision parts are completed in a single setup, with glass scales on every axis and a Fanuc 31i-B5 control driving five simultaneous axes. A 50-station high-speed ATC keeps it cutting; probing, scales, and a chip conveyor all come standard. Built in Japan by Hasegawa and supplied under Expand's GEN MILL brand — Japanese precision through one accountable source.
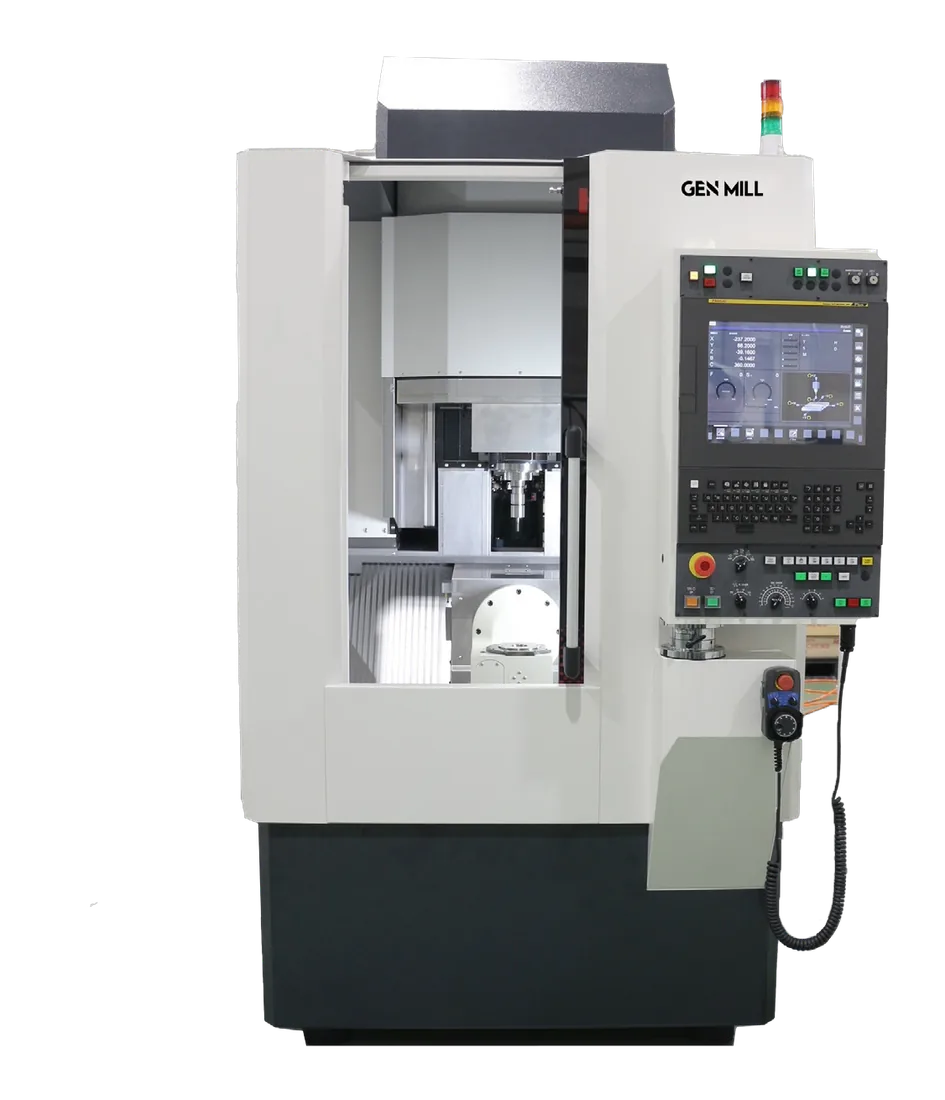
- ✓Mill and turn in one setup. Optional 2,000 RPM turning means turned and milled features finish on the same machine — no second op, no re-fixturing.
- ✓True 5-axis precision. 150 mm trunnion rotary table, tilt −20°/+120°, driven by a Fanuc 31i-B5 for five simultaneous axes.
- ✓High-speed built-in spindle. 25,000 RPM standard (45,000 RPM optional), HSK-E40 taper for fine, fast surface work.
- ✓Accuracy you can trust. Glass scales on all axes plus tool and part probing — included, not optional.
- ✓Productive and compact. 50-station HSK-E40 ATC at 1.9 s tool-to-tool, chip conveyor included, in a footprint that fits tight floor plans.
Small, complex, high-precision parts — medical, aerospace, and micro-components — the Hasegawa-built PM320 5-axis center finishes complete with live turning, holding roundness to 1 µm and Ra 0.1 µm finishes.

A pair of PM320-5X-T machining centers paired with integrated automation — loaded, run, and unloaded without an operator. The compact footprint makes a two-machine, lights-out cell practical even on a tight floor plan.
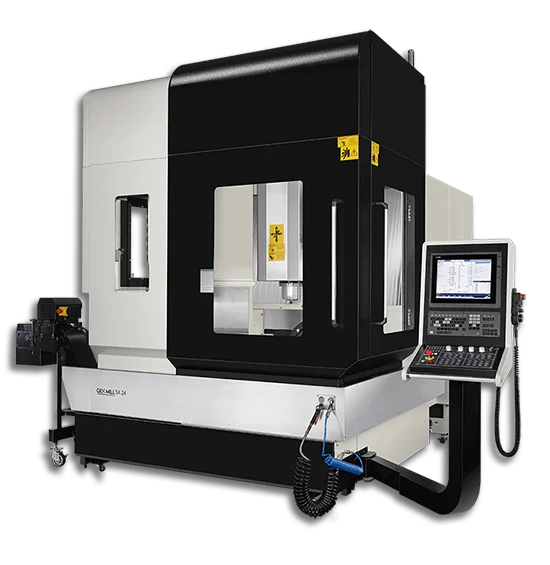
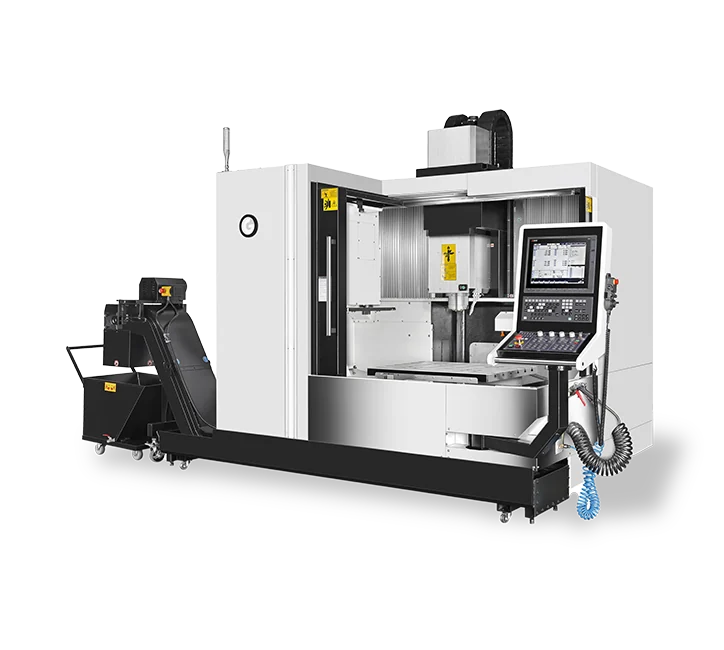
Ten vertical machining centers — five-axis trunnion machines from a Ø5.91″ platter up to Ø25.6″, a four-model 3-axis platform reaching 63″ of X travel, and a double-column bridge machine built like a CMM. Glass scales on the rotary axes as well as the linear ones, so position is measured at the table rather than inferred from the servo.

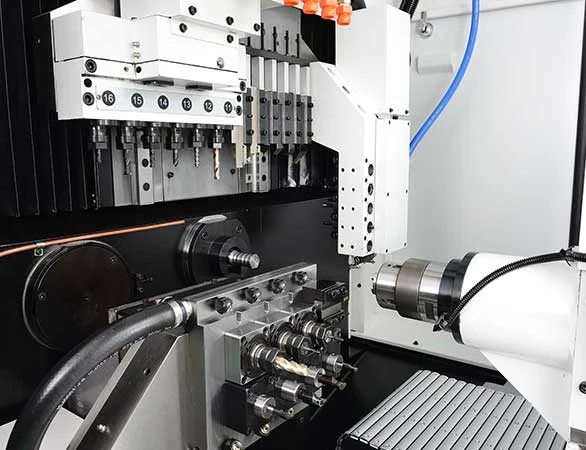
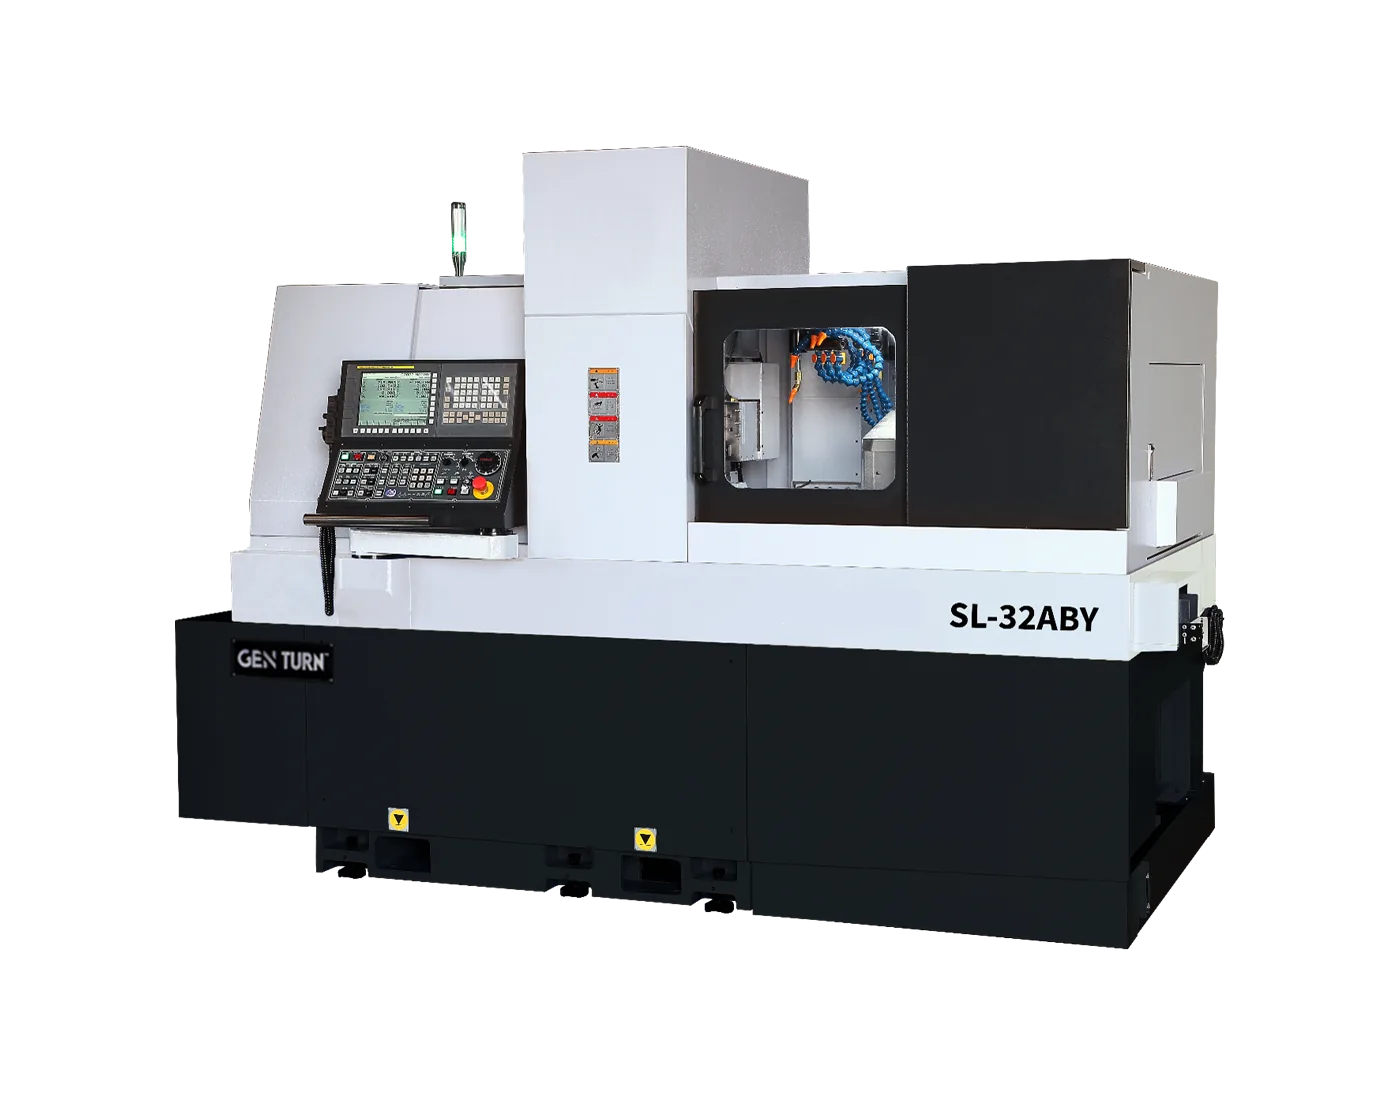
Five sliding-headstock machines from 20 mm to 2″ bar — guide-bushing, guide-bushing-less and hybrid builds that run either way. Driven tooling on every model, and a programmable B axis on the newest, the SL-32ABY.

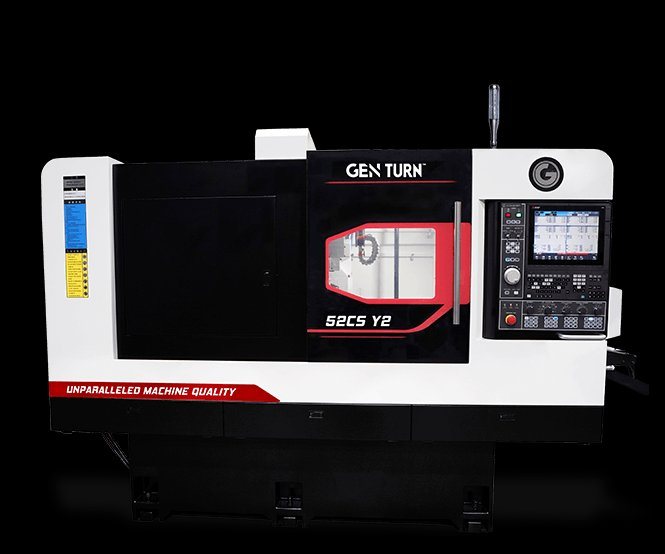
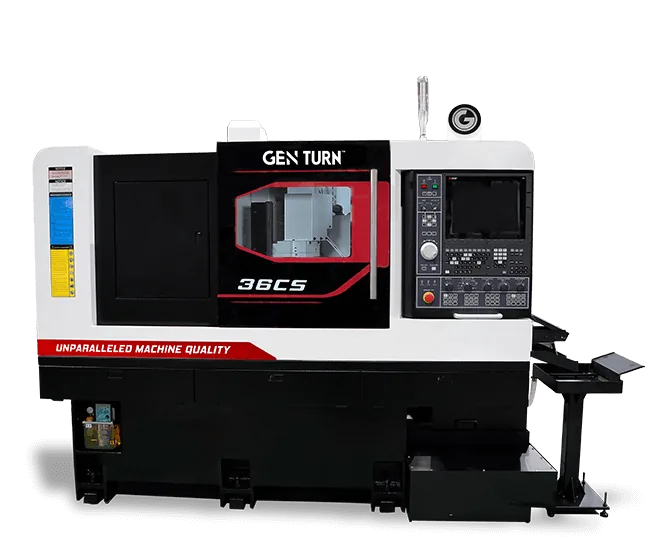
Beyond the Swiss range, two machines answer different problems. The 52-BY2 puts a twelve-tool “B” axis over twin opposed spindles, milling at any angle on both ends of the part. The C24 G runs small turned parts and fasteners unattended off a built-in gantry loader. GenTurn also builds the gang-tooled 32-GT and 52-GTS — listed in the specification table below.
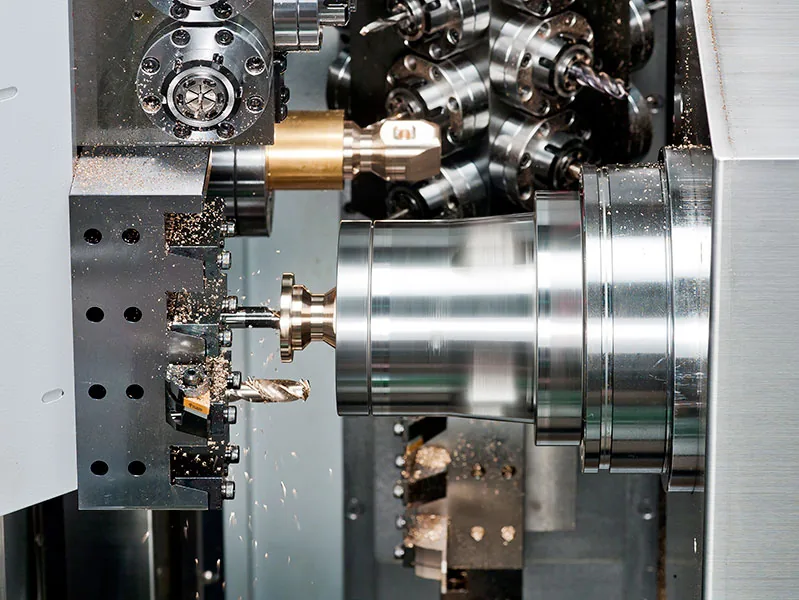
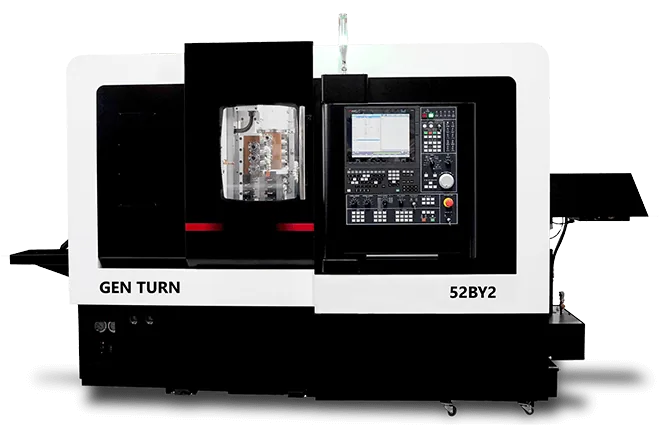
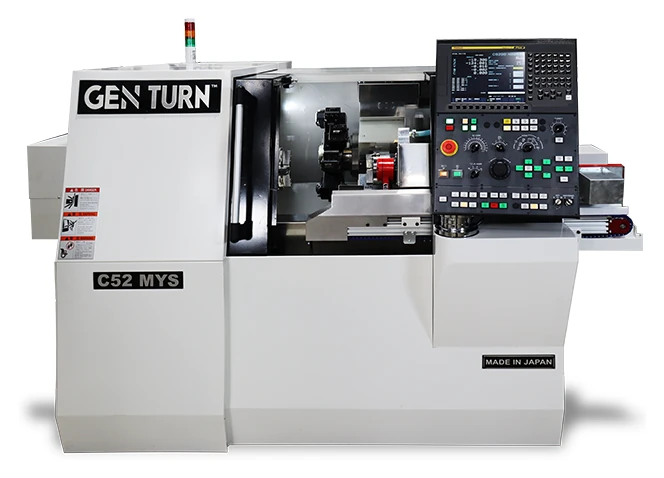
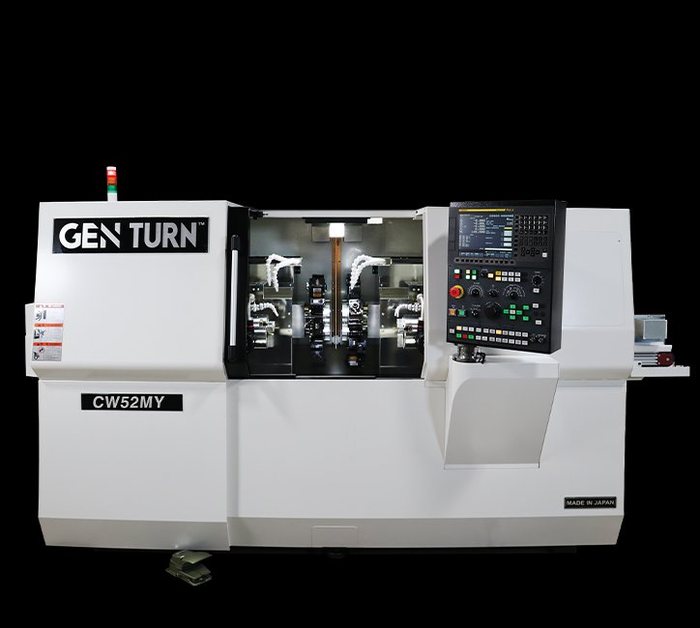
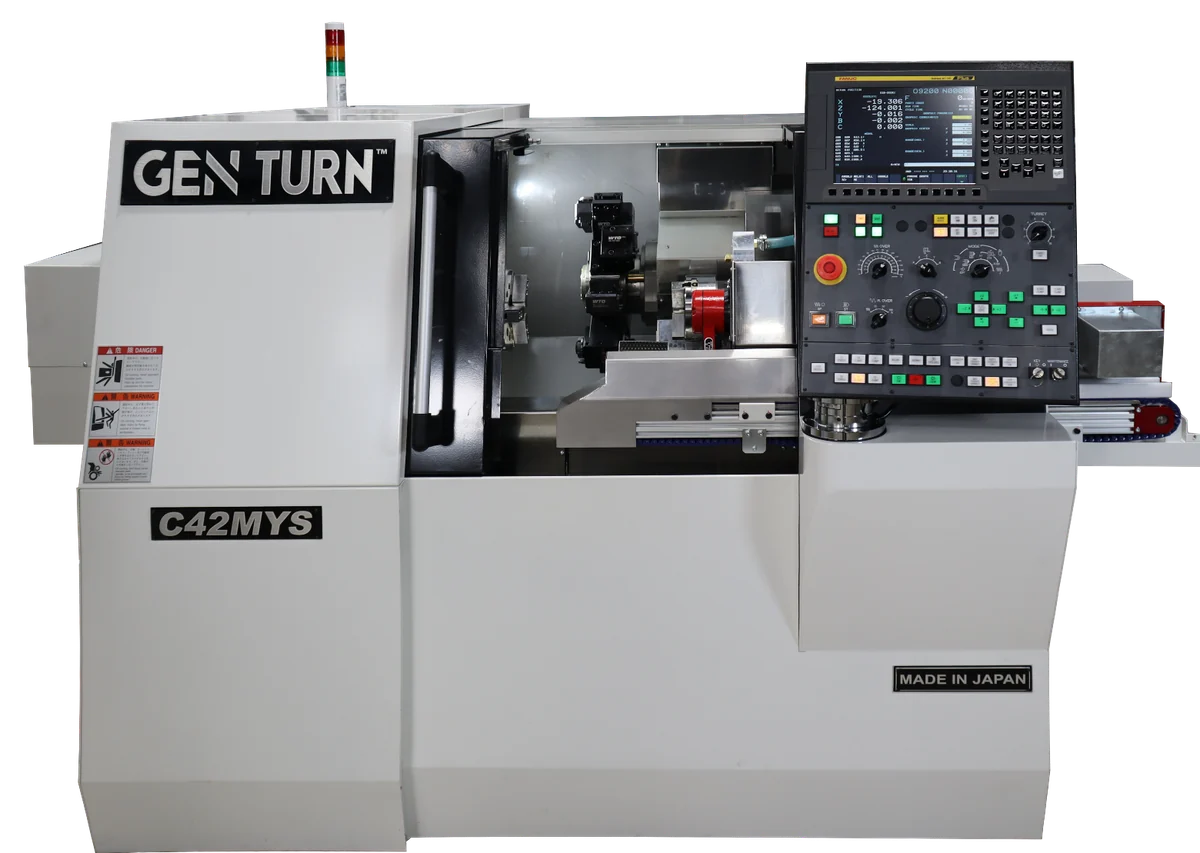
Seven twin-spindle turn-mill machines from 42 mm bar to 3″ chucking — five of them built in Japan by Hasegawa. Live turrets from 12 to 32 stations, Y axis throughout, a programmable B axis on the 52-BY2, and a built-in gantry loader on the CW52MY GII.
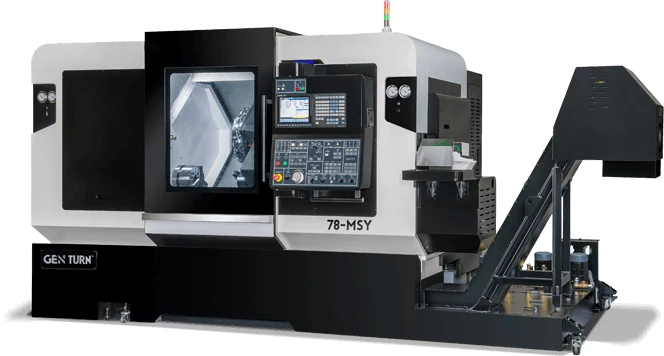
- ✓78 mm (3″) bar, twin opposed spindles. 4,000 RPM main and sub with full C-axis on both — complete front and back work in one cycle.
- ✓16-station BMT-65 live turret. Each station mounts multiple tools; a “Y” axis (±1.968″) handles off-centerline milling.
- ✓Heavy metal removal. A 30-HP integral refrigerated main spindle and 15-HP integral sub spindle hold size in tough material.
- ✓Big turned-and-milled parts, complete. Up to Ø12.79″ turning diameter and 22.04″ turning length — finished in one machine, not three.
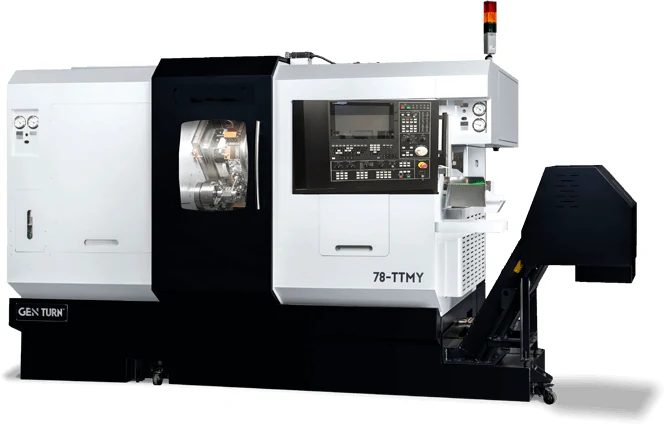
- ✓Twin 16-tool turrets — 32 driven positions. Each station mounts multiple tools, for the tooling capacity complex parts demand.
- ✓Glass scale feedback on X1 & X2. Direct positioning accuracy for tight-tolerance turned-and-milled work.
- ✓Simultaneous main & sub machining. Twin 4,000 RPM opposed spindles with full C-axis on both — front and back at the same time.
- ✓“Y” axis, 3.936″ travel. Deep off-centerline milling on 78 mm (3″) bar — complete parts, done-in-one.
Swiss-type sliding headstock, guide-bushing-less, gang-tooled, twin-turret turn-mill, B-axis nine-axis, and large-capacity 3″ bar work — the whole GEN TURN family side by side, so you can size the machine to the part instead of the other way around.
| Model | Bar capacityin / mm | Spindlerpm main / sub | Powerhp main / sub | Tool positions | Rapidsipm | Weightlb |
|---|---|---|---|---|---|---|
| C24 GTurning center · Japan | 1.00 / 25 | 6,000 | 7 | 8-station turret | 468 | 3,087 |
| C52 MYS6-axis turn-mill · Japan | 2.04 / 52 | 5,000 | 12 / 10 | 12 live stations | 787 | 8,377 |
| CW52 MY8-axis twin turret · Japan | 2.04 / 52 | 5,000 | 12 | 2 × 12 live | 787 | 10,584 |
| CW52MY GII8-axis + gantry · Japan | 2.04 / 52 | 5,000 | 12 | 2 × 12 live | 787 | 11,220 |
| SL-20Y28-axis Swiss | 0.79 / 20 | 10,000 / 8,000 | 5 | 30 (8 driven) | 944 | 5,954 |
| SL-32ABY7-axis Swiss · B-axis | 1.26 / 32 | 6,000 | 7.5 | 41 (13 driven) | 1,181 | 10,960 |
| SL-42Y28-axis Swiss | 1.65 / 42 | 6,000 | 10 | 33 (9 driven) | 944 | 11,024 |
| 32-GTGang-tooled lathe | 1.25 / 32 | 6,000 | 7.5 | Gang plate (turret opt.) | 787 | 4,850 |
| 36-CS7-axis Swiss | 1.375 / 36 | 6,000 | 10.6 | 27 (11 driven) | 1,181 | 8,818 |
| 52-CS Y28-axis Swiss | 2.00 / 51 | 6,000 | 15 | 33 (13 driven) | 1,181 | 13,880 |
| 52-GTS6-axis dual gang | 2.05 / 52 | 6,000 | 15 | Dual gang slides | 1,181 | 9,922 |
| 52-BY29-axis mill/turn | 2.01 / 51 | 6,000 | 15 | 36 (18 driven) | 1,181 | 12,345 |
| 78-MSY6-axis mill/turn | 3.07 / 78 | 4,000 | 30 / 15 | 16-station BMT-65 | 1,574 Z | 17,650 |
| 78-TTMY8-axis mill/turn | 3.07 / 70 | 4,000 | 30 / 20 | 2 × 16 BMT-65 | 1,573 Z | 22,751 |
Expand Machinery Robotics — Turnkey Automation
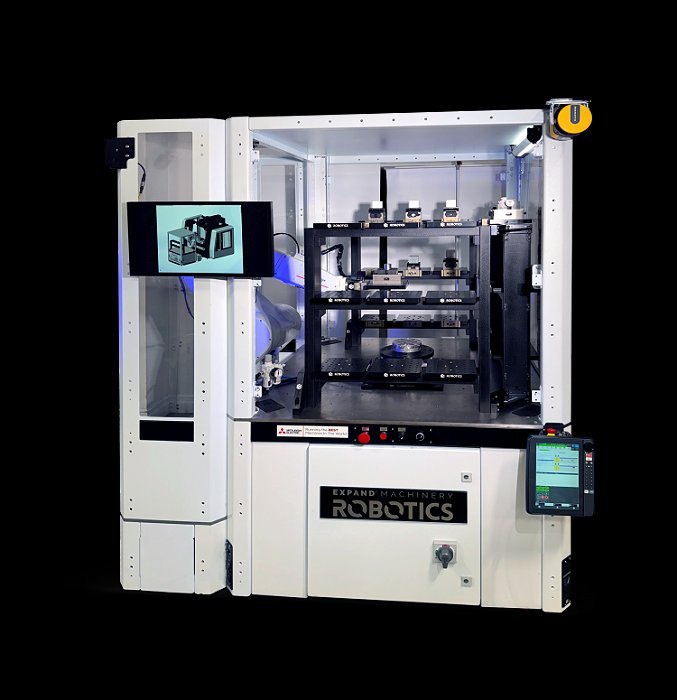
The Expand Machinery Robotics cell pairs directly with GenTurn and GenMill machines to deliver fully unattended production. Mitsubishi collaborative robot arm, precision fixture staging, and a monitoring display so your shop runs lights-out while you're not there.

An aerospace shop already running
lights-out — and tripling output.
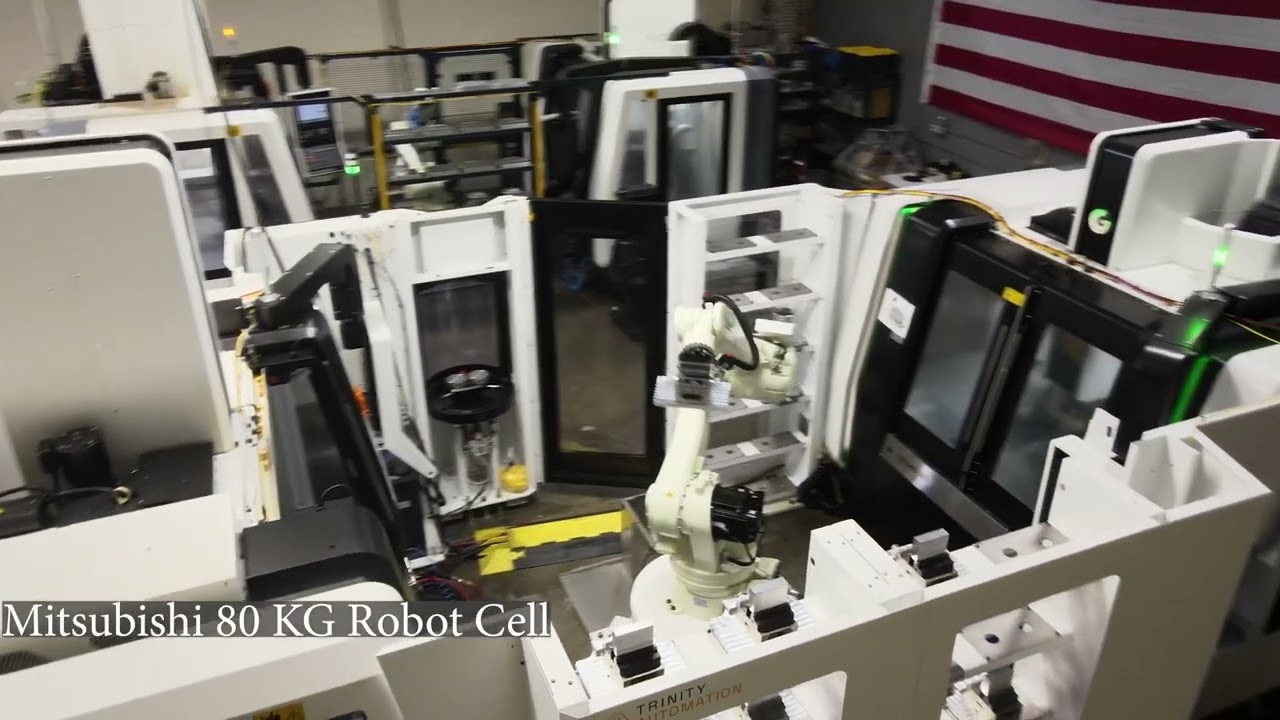
TL Aerotek — a precision aerospace job shop and longtime Expand Machinery customer — needed to keep up with surging demand without taking on labor uncertainty. Expand engineered and integrated a Mitsubishi Electric LoadMate Plus cell (an RV20 six-axis robot with a Schunk quick-change pallet system) onto the shop's GEN MILL 5X-12. Because the machine already ran a Mitsubishi CNC, the robot connects over a single Ethernet link and is programmed in G-code from the same screen as the machine — no separate robot expertise needed. It's the exact GEN MILL and automation platform LOMA brings to Northeast shops.
“Both companies give me what I need: super support, performance, and reliability.”Tai Le · Owner, TL Aerotek
Machines
CNC Swiss lathes Turn-mill & multi-axis Multi-turret lathes Gang-tooled & production Turn-grind Ultra-precision turning Vertical machining centers 5-axis machining centers Nano-precision mold Sawing & cutoff Machine selectorApplications
Aerospace & defense Medical & orthopedic Lights-out machining All machines — index HomeTalk to us
978·356·2500Send us the part — material, tolerance and volume — and we will tell you which machine fits, or that none of them do.
Send us the part → Tooling & workholding — NSIT →Send us the part.
Tell us the material, the tolerance and the volume and we will tell you which of these fits — or that none of them do. Send us the part →