Request free assessment →
Ready to run lights out? flip the switch
Single-source industrial partner

Your shop. Fully equipped. Fully supported.

Machines. Tooling. Application Support. All in.

We supply the CNC machinery, spec the cutting tools, and provide full application engineering and CNC programming support — so your shop runs the way it was built to.

3
Capabilities · one partner
1
Call to solve it all
0
Gaps in your supply chain
Lights-out potential
Builder partnerships

Ultra-precision machinery.
Built for lights-out production.

LOMA represents four premium machine builder lines chosen specifically for their capability in ultra-precision, high-productivity, and lights-out-ready manufacturing. Every machine we supply is backed by full application engineering, verified tooling, and on-site programming support — from day one. We partner with aerospace, defense, and precision manufacturers across the Northeast.

Machine categories
Industries served
Aerospace Defense Medical Semiconductor Optics Space & Satellite Energy Precision Mechanics
Swiss CNC · Twin-spindle turning · 5-axis GEN MILL VMC
Expand Machinery
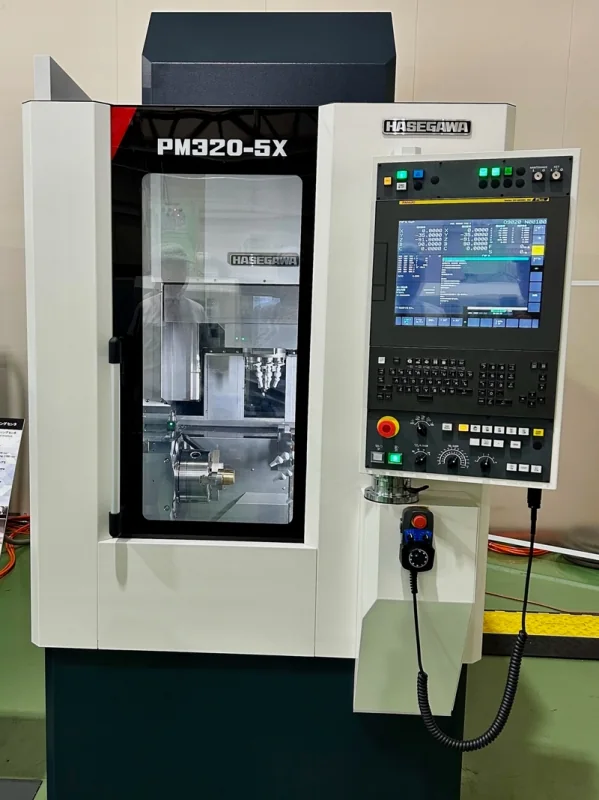
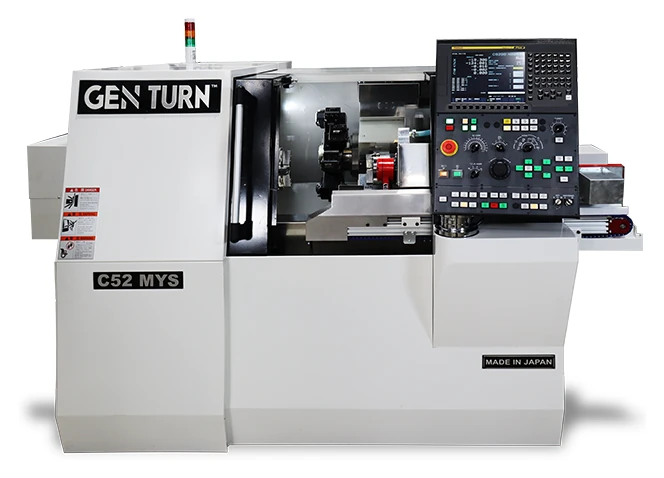
Expand Machinery builds the GenTurn Swiss and twin-spindle turning centers and the GEN MILL series of high-speed, high-accuracy machining centers — including our featured machine, the PM320-5X-T 5-axis super-precision compact VMC with live turning. Select models — the PM320-5X, GenTurn CW52 MY, C52 MYS, and C24 G — are built in Japan by Hasegawa, with in-stock inventory for immediate delivery. The most capable accessible precision platform in the market.
expandmachinery.com ↗
Featured machine
Made in JapanHasegawa
PM320-5X-T
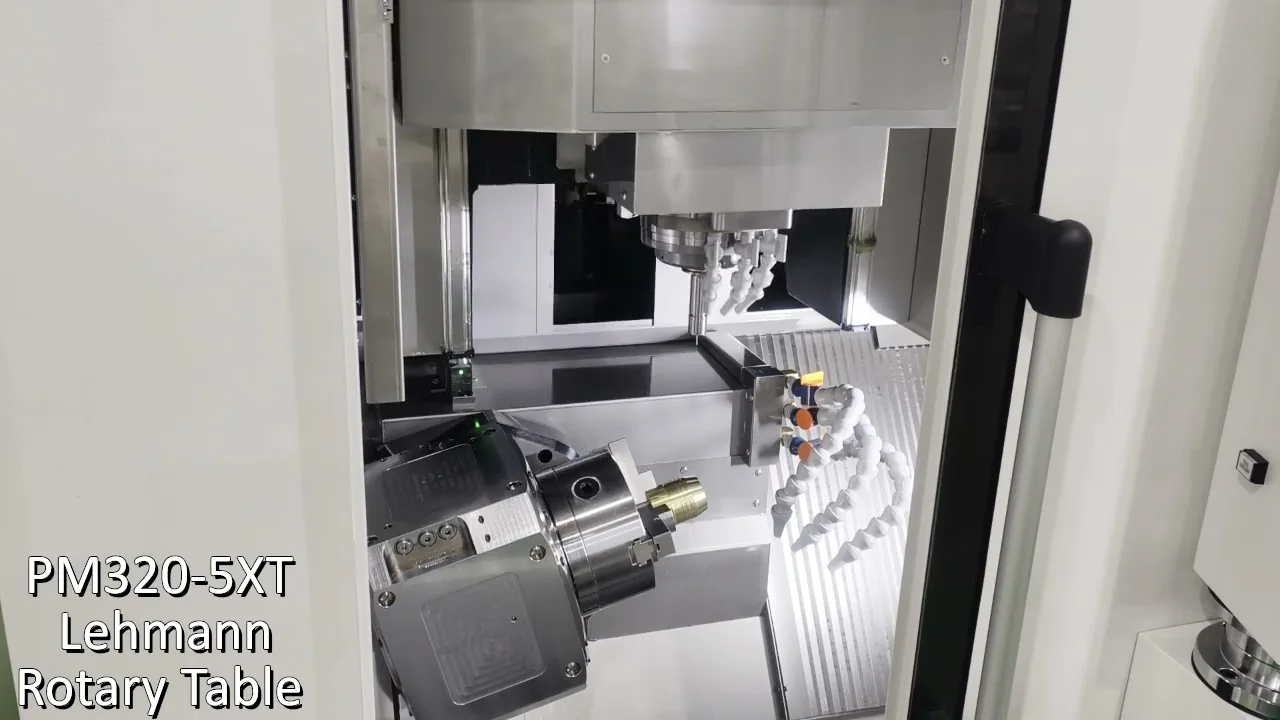
5-Axis Super-Precision Compact VMC — with live turning
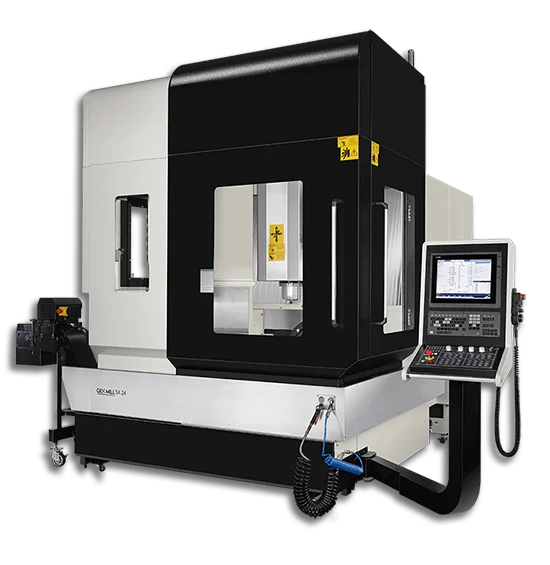
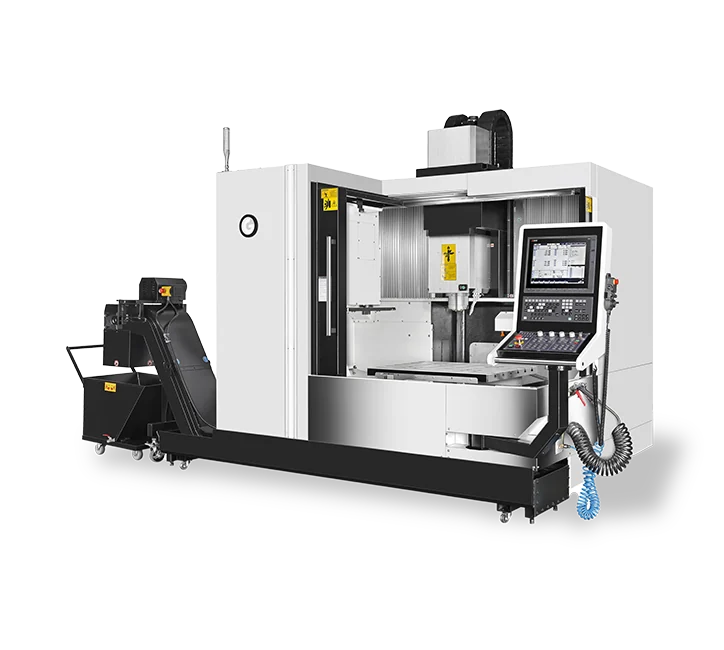
PM320-5X-T — 5-Axis Super-Precision VMC
Expand Machinery · GEN MILL · official

One compact machine that mills in full 5-axis and turns. The PM320-5X-T pairs a 25,000 RPM built-in spindle with a 2,000 RPM turning capability on a 150 mm trunnion table — so complex precision parts are completed in a single setup, with glass scales on every axis and a Fanuc 31i-B5 control driving five simultaneous axes. A 50-station high-speed ATC keeps it cutting; probing, scales, and a chip conveyor all come standard. Built in Japan by Hasegawa and supplied under Expand's GEN MILL brand — Japanese precision through one accountable source.
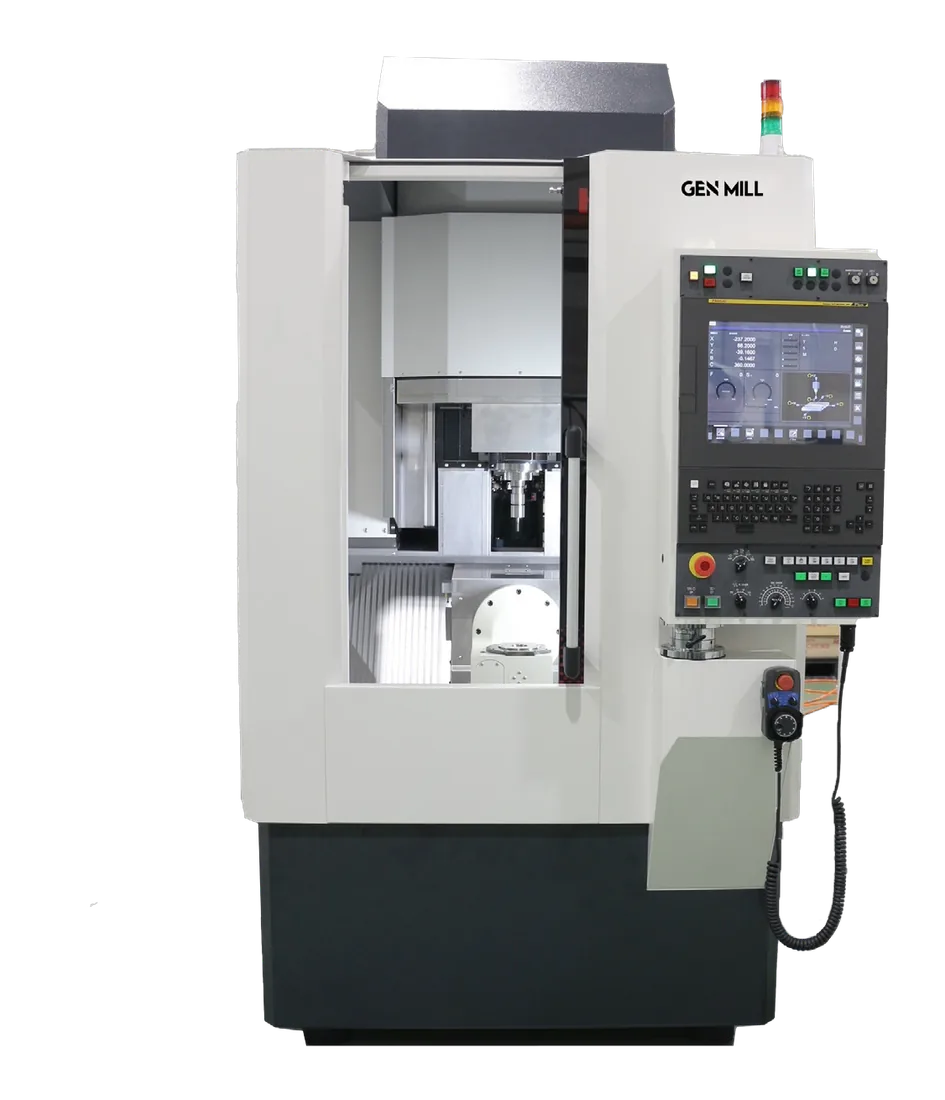
Made in Japan 5-axis simultaneous 2,000 RPM turning 25,000 RPM spindle 50-tool ATC Glass scales Fanuc 31i-B5
Expand Machinery PM320-5X-T GEN MILL 5-axis compact VMC
  • Mill and turn in one setup. Optional 2,000 RPM turning means turned and milled features finish on the same machine — no second op, no re-fixturing.
  • True 5-axis precision. 150 mm trunnion rotary table, tilt −20°/+120°, driven by a Fanuc 31i-B5 for five simultaneous axes.
  • High-speed built-in spindle. 25,000 RPM standard (45,000 RPM optional), HSK-E40 taper for fine, fast surface work.
  • Accuracy you can trust. Glass scales on all axes plus tool and part probing — included, not optional.
  • Productive and compact. 50-station HSK-E40 ATC at 1.9 s tool-to-tool, chip conveyor included, in a footprint that fits tight floor plans.
Configuration
5-axis + turning
Spindle
25,000 RPM · HSK-E40
Turning
2,000 RPM (5X-T)
Control
Fanuc 31i-B5
ATC
50 tools · 1.9 s
Travels X/Y/Z
320·340·380 mm
Trunnion table
Ø100 mm · −20/+120°
Footprint
1.2×2.7 m · 4,100 kg
Workpiece samples · Hasegawa PM320 (GEN MILL)

Small, complex, high-precision parts — medical, aerospace, and micro-components — the Hasegawa-built PM320 5-axis center finishes complete with live turning, holding roundness to 1 µm and Ra 0.1 µm finishes.
Hasegawa PM320 GEN MILL machined workpiece sample
Representative parts produced on the Hasegawa-built GEN MILL PM320.
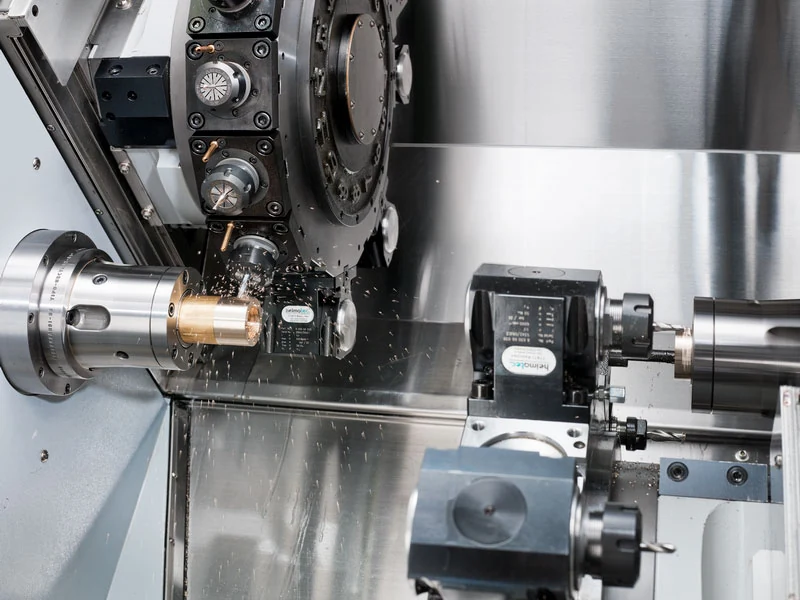
Expand · PM320 automation Two Expand PM320-5X-T 5-axis machines paired with integrated robotic automation
Lights-out · integrated automation
Two PM320-5X-T’s, running unattended.

A pair of PM320-5X-T machining centers paired with integrated automation — loaded, run, and unloaded without an operator. The compact footprint makes a two-machine, lights-out cell practical even on a tight floor plan.

Swiss machining up to 2" diameter.
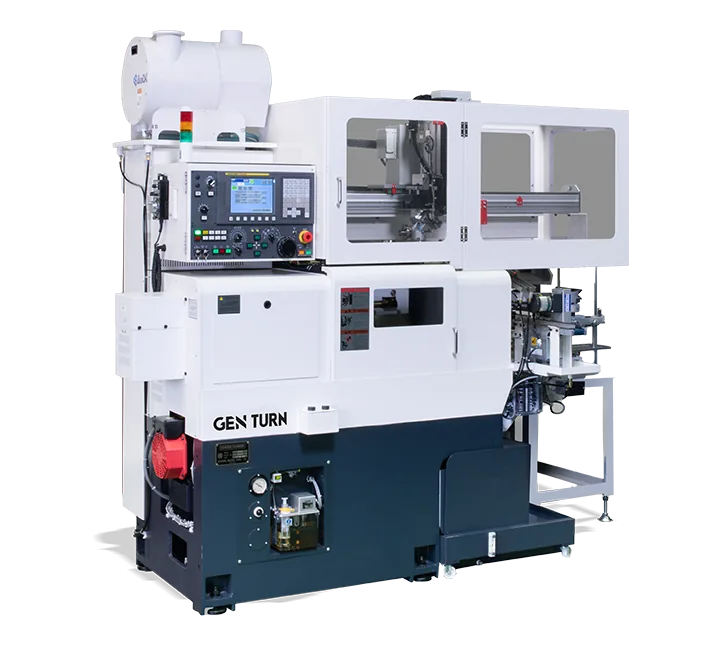
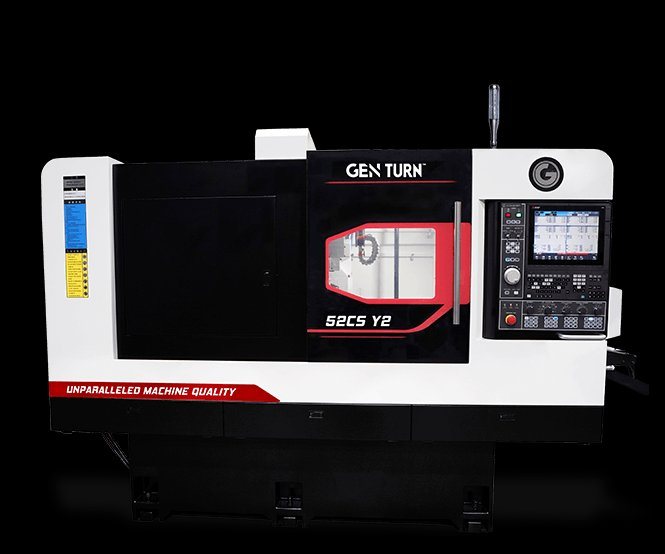
GenTurn 52CS Y2 — Swiss CNC Screw Machine
Expand Machinery · official demo
GenTurn 52CS Y2 — Swiss-type CNC
Swiss precision turning — up to ~2" (52mm) bar.
Swiss-type CNC screw machine with Y-axis for long, slender, high-tolerance parts up to roughly 2 inch (52mm) bar. Sub-spindle and live tooling for complete parts in a single cycle.
Swiss-typeY-axis~52mm barSub-spindle
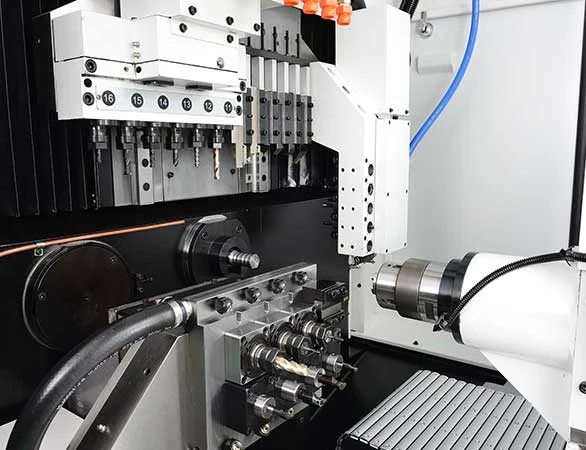
GenTurn 52CS gang tooling inside the work area
GenTurn 52CS — gang tooling inside
GenTurn 52CS Y2 Swiss CNC machine
GenTurn 52CS Y2 — Swiss CNC screw machine
CNC Swiss screw machine
GenTurn CS / CW Series
Multi-axis CNC Swiss-type machines with Y-axis, live tooling, sub-spindle, and B-axis milling. Simultaneous front and back working for complete part production in a single pass. Built for medical, aerospace, and defense precision components.
Swiss CNCY-axis + live toolingSub-spindle20–52mm bar
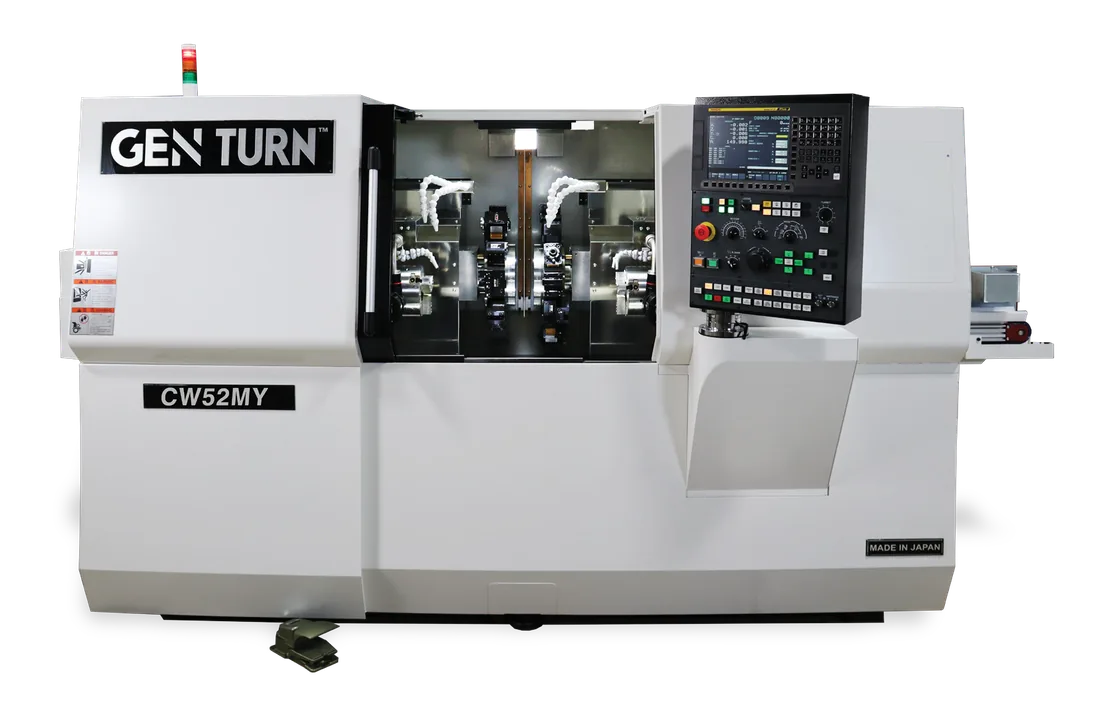
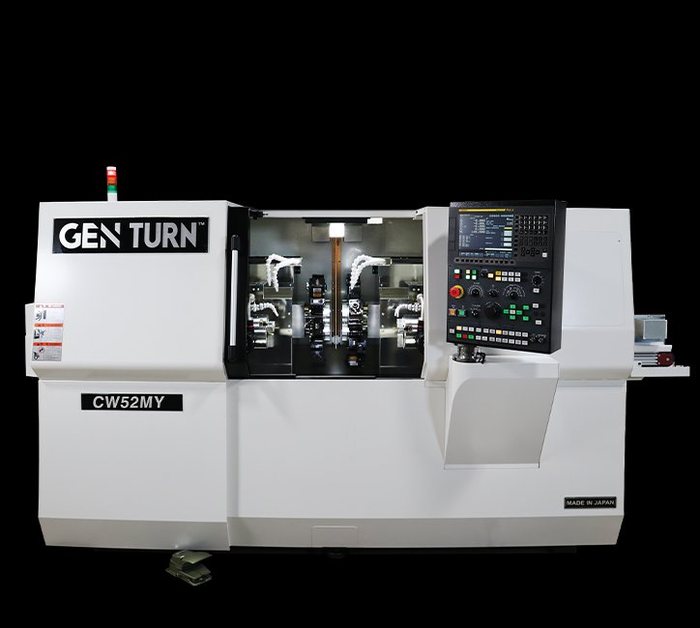
GenTurn CW52MY twin-spindle turning center
GenTurn CW52MY — twin spindle · Made in Japan
Twin-spindle turning center
GenTurn CW52MY
Compact twin-spindle CNC turning center with Y-axis milling. Dual spindle simultaneous operation with full milling capability — dramatically reducing cycle time on complex turned parts with secondary operations. Made in Japan.
Twin spindleY-axis millingMade in JapanCompact footprint
Swiss-type rangeGenTurn SL / CS · 20–51 mm bar

Five sliding-headstock machines from 20 mm to 2″ bar — guide-bushing, guide-bushing-less and hybrid builds that run either way. Driven tooling on every model, and a programmable B axis on the newest, the SL-32ABY.

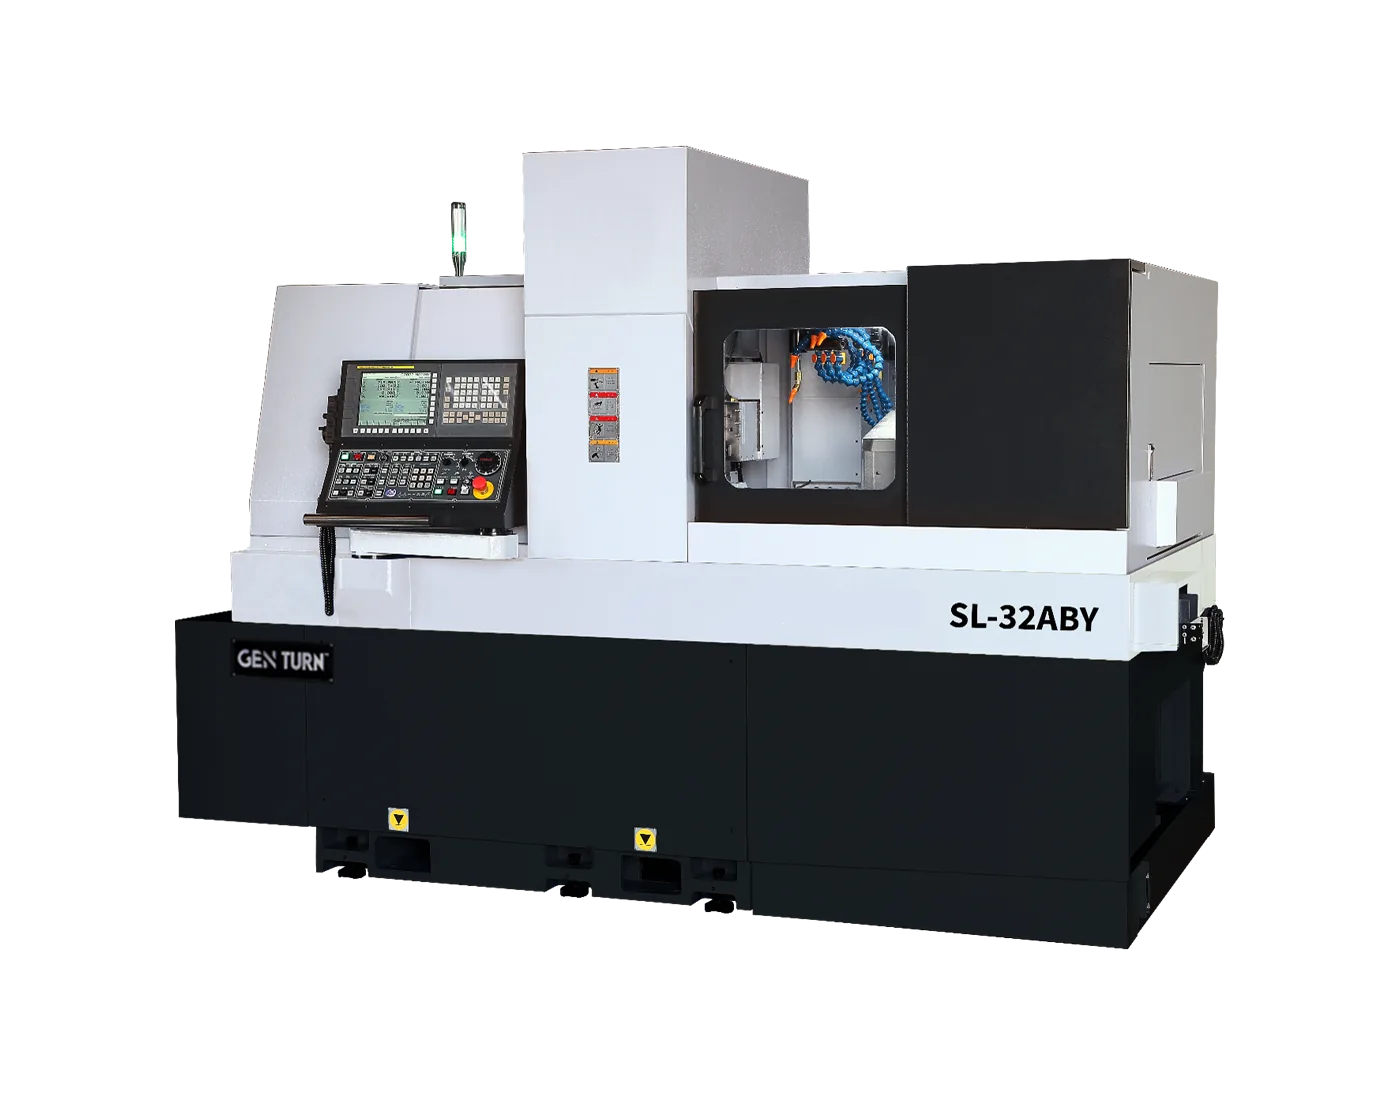
SL-32ABY — hybrid Swiss with full B axis
Expand Machinery · new for 2026
New for 2026 · 32 mm hybrid Swiss
A Swiss lathe that mills at any angle.
Four fully programmable B-axis live tools work at any angle on both main and sub spindle, so features that used to need a second operation come off complete. Hybrid means you choose per job — run 32 mm bar with the rotary guide bushing for long slender work, or pull it and run chucker-style to kill remnant waste on short parts.
41 tools / 13 drivenB-axis any angleGuide bushing optionalMitsubishi M-830
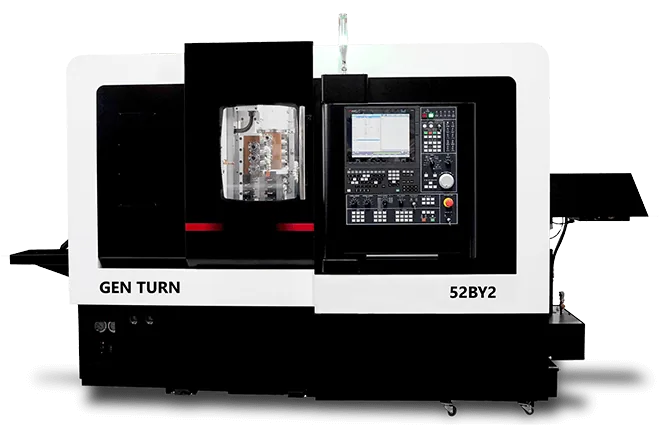
B-axis & production lathesGenTurn 52-BY2 · C24 G

Beyond the Swiss range, two machines answer different problems. The 52-BY2 puts a twelve-tool “B” axis over twin opposed spindles, milling at any angle on both ends of the part. The C24 G runs small turned parts and fasteners unattended off a built-in gantry loader. GenTurn also builds the gang-tooled 32-GT and 52-GTS — listed in the specification table below.
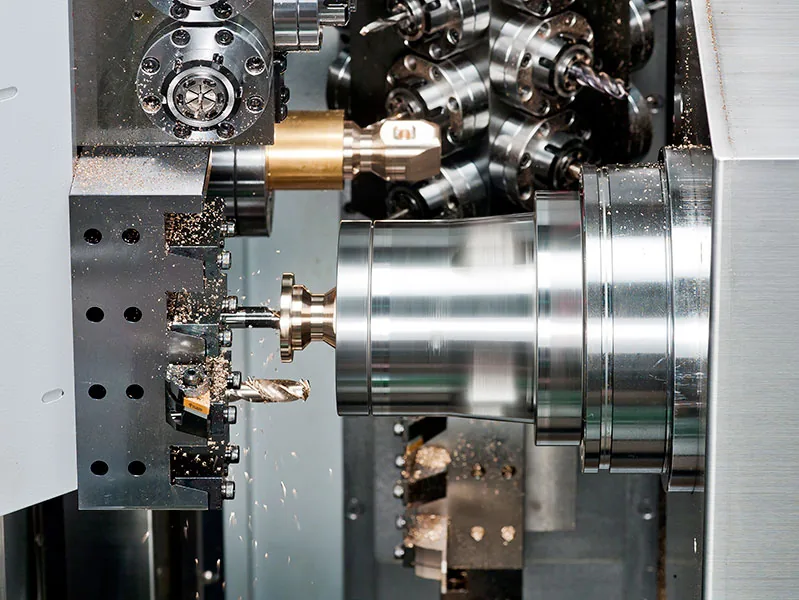
GenTurn 52-BY2 B-axis tooling cutting a turned part
52-BY2 — B-axis live tooling working off centerline
Why a B-axis
Any angle, both ends, one setup.
Live tooling fixed on centerline can only drill and mill square to the part. A programmable B-axis swings the driven tool to any angle — angled holes, off-axis pockets, compound features — and on the 52-BY2 those twelve B-axis tools serve the main and sub spindle both. Features that would otherwise mean a second operation on a mill get cut while the bar is still in the collet.
Turn-mill rangeGenTurn C / CW / 78 · 42–78 mm bar

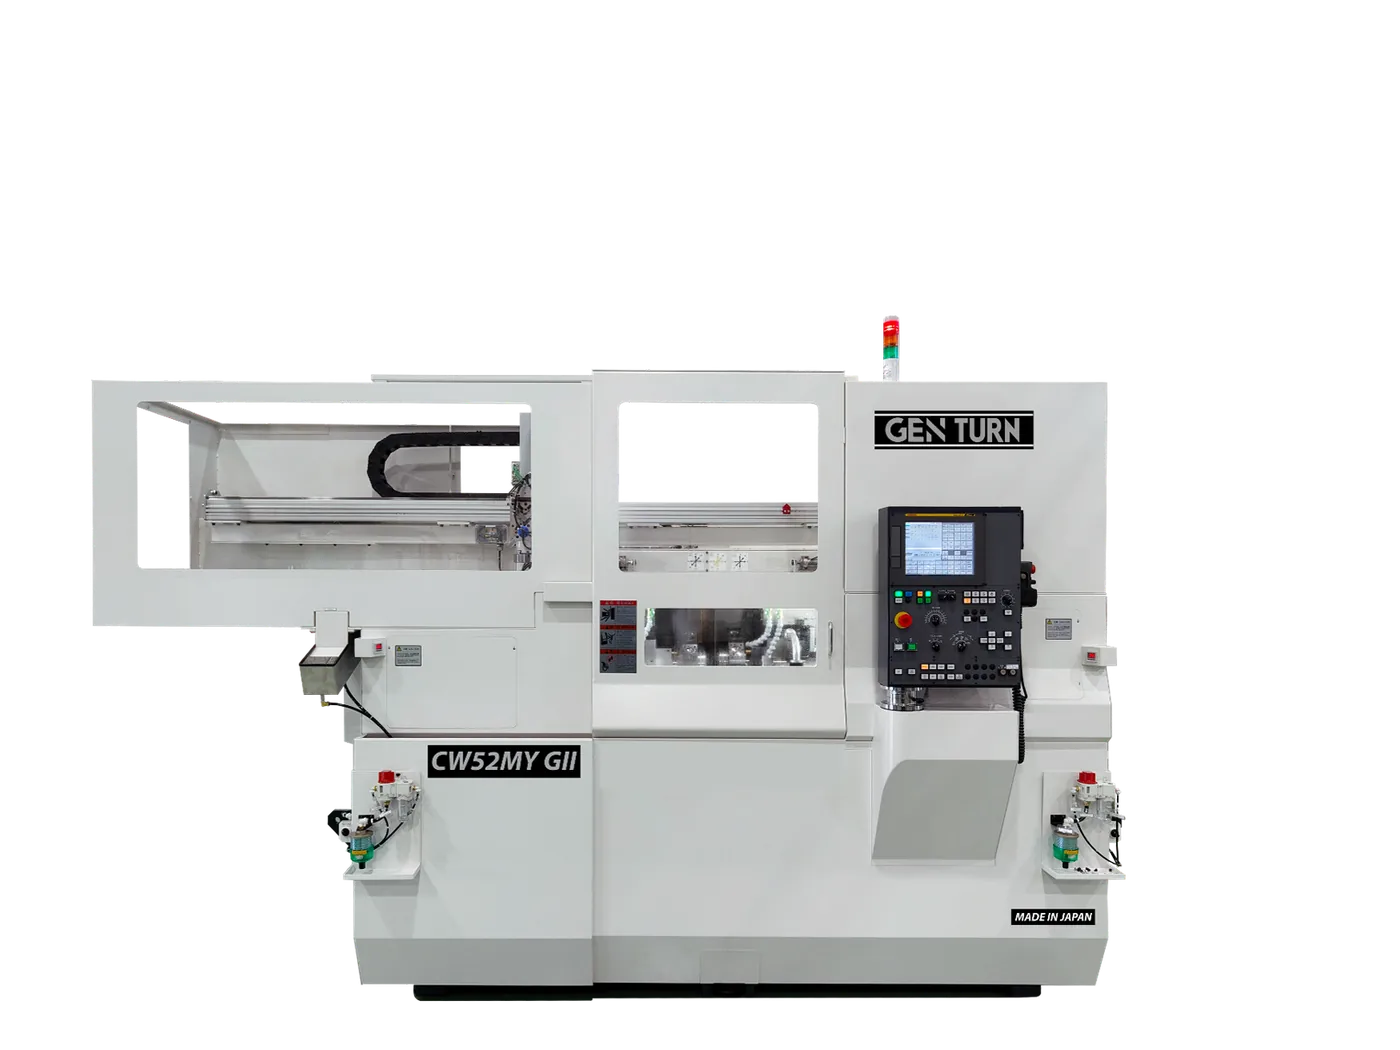
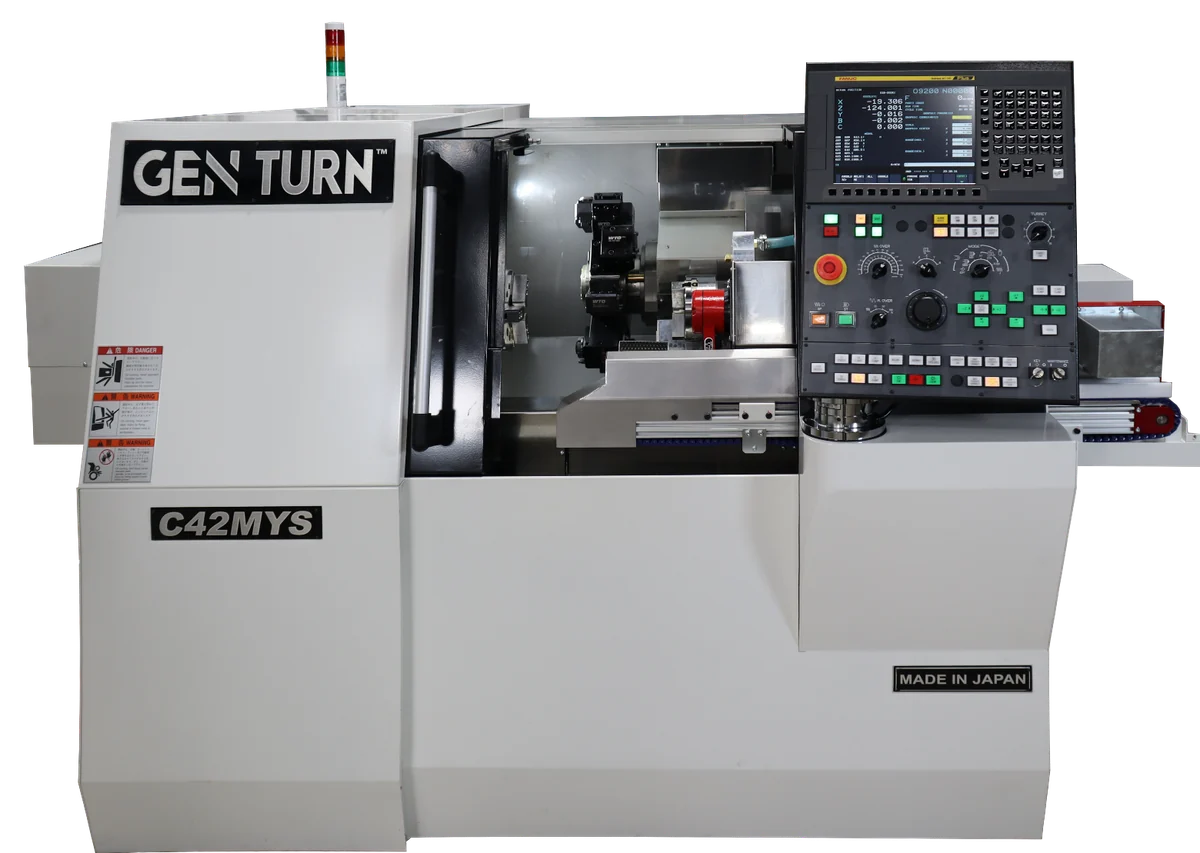
Seven twin-spindle turn-mill machines from 42 mm bar to 3″ chucking — five of them built in Japan by Hasegawa. Live turrets from 12 to 32 stations, Y axis throughout, a programmable B axis on the 52-BY2, and a built-in gantry loader on the CW52MY GII.
Workpiece samples · Hasegawa C-series
Hasegawa C-series machined workpiece sample
Representative parts produced on the Hasegawa-built GEN TURN C-series (C24 through CW52).
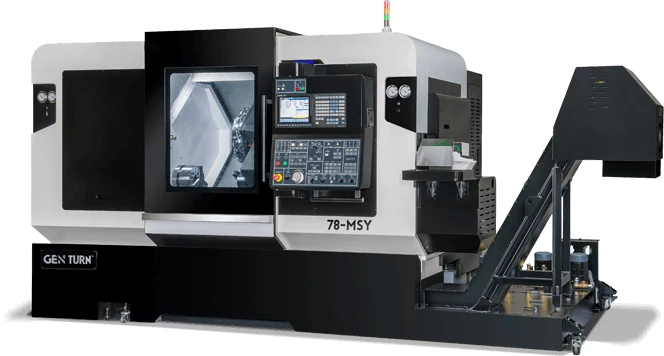
Large-capacity turn-millGenTurn 78 Series · 3″ bar · twin opposed spindles
GenTurn 78-MSY 6-axis mill/turn lathe with 16-tool turret
  • 78 mm (3″) bar, twin opposed spindles. 4,000 RPM main and sub with full C-axis on both — complete front and back work in one cycle.
  • 16-station BMT-65 live turret. Each station mounts multiple tools; a “Y” axis (±1.968″) handles off-centerline milling.
  • Heavy metal removal. A 30-HP integral refrigerated main spindle and 15-HP integral sub spindle hold size in tough material.
  • Big turned-and-milled parts, complete. Up to Ø12.79″ turning diameter and 22.04″ turning length — finished in one machine, not three.
Config
6-axis mill/turn · 16-tool turret
Bar capacity
3″ 78 mm · A2-6
Spindles
Twin 4,000 RPM · full C main+sub
Turret
16 station BMT-65 live
78-MSY · 6-axis mill/turn
View the 78-MSY on Expand ↗
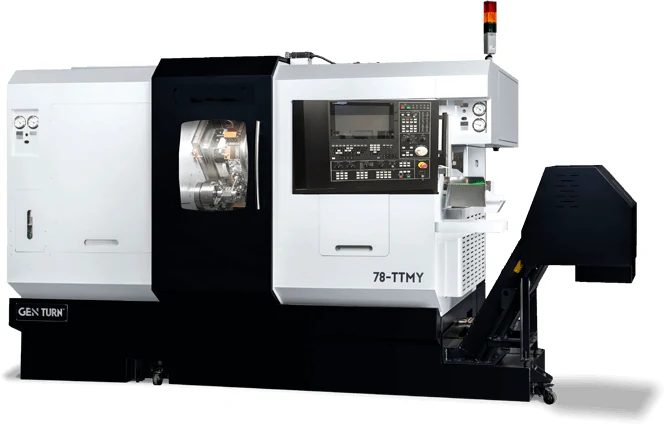
GenTurn 78-TTMY 8-axis mill/turn lathe with twin 16-tool turrets
  • Twin 16-tool turrets — 32 driven positions. Each station mounts multiple tools, for the tooling capacity complex parts demand.
  • Glass scale feedback on X1 & X2. Direct positioning accuracy for tight-tolerance turned-and-milled work.
  • Simultaneous main & sub machining. Twin 4,000 RPM opposed spindles with full C-axis on both — front and back at the same time.
  • “Y” axis, 3.936″ travel. Deep off-centerline milling on 78 mm (3″) bar — complete parts, done-in-one.
Config
8-axis mill/turn · twin turrets
Bar capacity
3″ 78 mm · A2-6
Driven tools
32 twin 16-station turrets
Feedback
Glass scales X1 & X2 axes
GenTurn 78-TTMY work area — twin turrets machining a part with live tooling
78-TTMY — twin-turret work area, simultaneous main & sub
78-TTMY · 8-axis, twin 16-tool turrets
View the 78-TTMY on Expand ↗
The full GEN TURN range
Twelve machines. 20 mm bar to 3″ chucking.

Swiss-type sliding headstock, guide-bushing-less, gang-tooled, twin-turret turn-mill, B-axis nine-axis, and large-capacity 3″ bar work — the whole GEN TURN family side by side, so you can size the machine to the part instead of the other way around.

Fourteen machines, drawn to scale
Swiss-type Turn-mill Gang / turning center
Bar length = maximum barstock diameter, to scale across the range. 20 mm through 78 mm.
SL-20Y28-axis Swiss
20 mm · 0.79″
10,000 rpm · 30 tools
5,954 lb
C24 GTurning center
25 mm · 1.00″
6,000 rpm · 8-stn turret
3,087 lb
32-GTGang-tooled
32 mm · 1.25″
6,000 rpm · gang plate
4,850 lb
SL-32ABYSwiss · B-axis
32 mm · 1.26″
6,000 rpm · 41 tools
10,960 lb
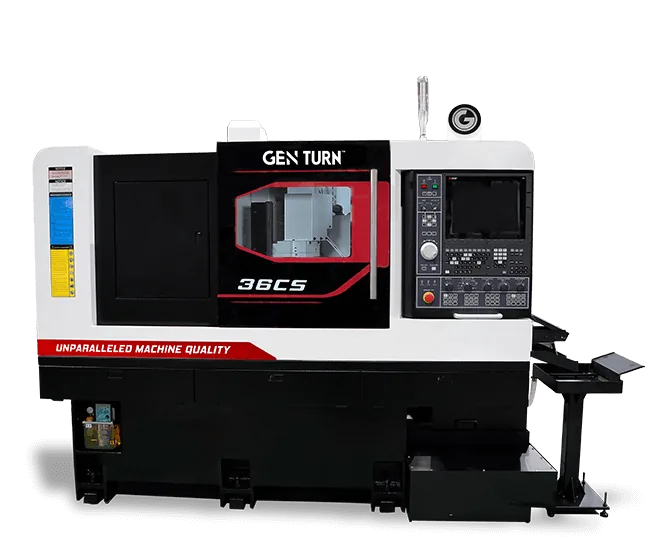
36-CS7-axis Swiss
36 mm · 1.38″
6,000 rpm · 27 tools
8,818 lb
SL-42Y28-axis Swiss
42 mm · 1.65″
6,000 rpm · 33 tools
11,024 lb
52-CS Y28-axis Swiss
51 mm · 2.00″
6,000 rpm · 33 tools
13,880 lb
52-BY29-axis mill/turn
51 mm · 2.01″
6,000 rpm · 36 tools
12,345 lb
C52 MYS6-axis turn-mill
52 mm · 2.04″
5,000 rpm · 12 live
8,377 lb
CW52 MY8-axis twin turret
52 mm · 2.04″
5,000 rpm · 2 × 12 live
10,584 lb
CW52MY GII8-axis + gantry
52 mm · 2.04″
5,000 rpm · 2 × 12 live
11,220 lb
52-GTSDual gang-tooled
52 mm · 2.05″
6,000 rpm · dual gang
9,922 lb
78-MSY6-axis mill/turn
78 mm · 3.07″
4,000 rpm · 16-stn BMT
17,650 lb
78-TTMY8-axis mill/turn
78 mm · 3.07″
4,000 rpm · 2 × 16 BMT
22,751 lb
0 mm20395878 mm
Capacity shown for the main spindle. The C24 G, C52 MYS, CW52 MY and CW52MY GII are built in Japan by Hasegawa Machine Works, as is the C42 MYS — available through Expand but not in the printed catalogue. Full specifications for every model in the table below and in the catalogue.
GEN TURN — Swiss, gang-tooled and mill-turnFourteen models · 20 mm bar to 3-inch chucking
Model Bar capacityin / mmSpindlerpm main / subPowerhp main / subTool positionsRapidsipmWeightlb
C24 GTurning center · Japan 1.00 / 256,00078-station turret4683,087
C52 MYS6-axis turn-mill · Japan 2.04 / 525,00012 / 1012 live stations7878,377
CW52 MY8-axis twin turret · Japan 2.04 / 525,000122 × 12 live78710,584
CW52MY GII8-axis + gantry · Japan 2.04 / 525,000122 × 12 live78711,220
SL-20Y28-axis Swiss 0.79 / 2010,000 / 8,000530 (8 driven)9445,954
SL-32ABY7-axis Swiss · B-axis 1.26 / 326,0007.541 (13 driven)1,18110,960
SL-42Y28-axis Swiss 1.65 / 426,0001033 (9 driven)94411,024
32-GTGang-tooled lathe 1.25 / 326,0007.5Gang plate (turret opt.)7874,850
36-CS7-axis Swiss 1.375 / 366,00010.627 (11 driven)1,1818,818
52-CS Y28-axis Swiss 2.00 / 516,0001533 (13 driven)1,18113,880
52-GTS6-axis dual gang 2.05 / 526,00015Dual gang slides1,1819,922
52-BY29-axis mill/turn 2.01 / 516,0001536 (18 driven)1,18112,345
78-MSY6-axis mill/turn 3.07 / 784,00030 / 1516-station BMT-651,574 Z17,650
78-TTMY8-axis mill/turn 3.07 / 704,00030 / 202 × 16 BMT-651,573 Z22,751
Bar capacity shown for the main spindle. Where two figures appear, the second is the sub spindle. Rapids are the fastest linear axis; on the 78-MSY and 78-TTMY that is Z (X is 630 ipm). The C24 G, C52 MYS, CW52 MY and CW52MY GII are built in Japan by Hasegawa Machine Works, as is the C42 MYS — available through Expand but not listed in the printed catalogue; ask us for specifications. Specifications per the 2026 GEN TURN catalogue, the SL-32ABY and CW52MY GII data sheets, and subject to change — confirm configuration on quote.
↓  2026 GEN TURN catalog (PDF) See the full GEN TURN lineup ↗
Lights-Out Automation Platform

Expand Machinery Robotics — Turnkey Automation

The Expand Machinery Robotics cell pairs directly with GenTurn and GenMill machines to deliver fully unattended production. Mitsubishi collaborative robot arm, precision fixture staging, and a monitoring display so your shop runs lights-out while you're not there.

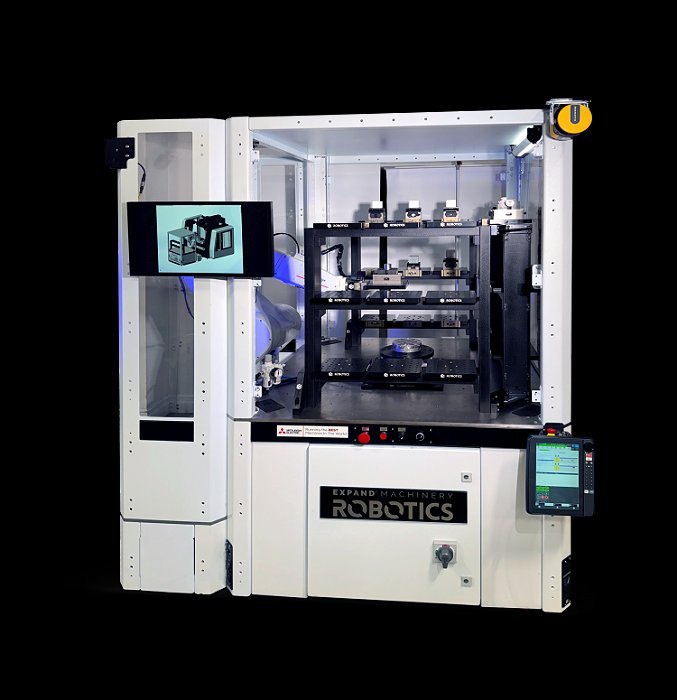
Expand Machinery Robotics — Lights-Out Automation
Official Expand Machinery · expandmachinery.com
Automation · Unattended production
Full lights-out robot cell — live demo
See the Expand Robotics cell in action: cobot arm loading and unloading a GenTurn Swiss machine, precision fixture staging, and continuous unattended production. The complete automation solution for high-mix precision manufacturing — engineered to run while no one's watching.
Mitsubishi cobot GenTurn integration High-mix capable Lights-out ready
Expand Machinery Robotics lights-out automation cell
Expand Machinery Robotics — lights-out cell
Field proof · Customer success

An aerospace shop already running
lights-out — and tripling output.

TL Aerotek — a precision aerospace job shop and longtime Expand Machinery customer — needed to keep up with surging demand without taking on labor uncertainty. Expand engineered and integrated a Mitsubishi Electric LoadMate Plus cell (an RV20 six-axis robot with a Schunk quick-change pallet system) onto the shop's GEN MILL 5X-12. Because the machine already ran a Mitsubishi CNC, the robot connects over a single Ethernet link and is programd in G-code from the same screen as the machine — no separate robot expertise needed. It's the exact GEN MILL and automation platform LOMA brings to Northeast shops.
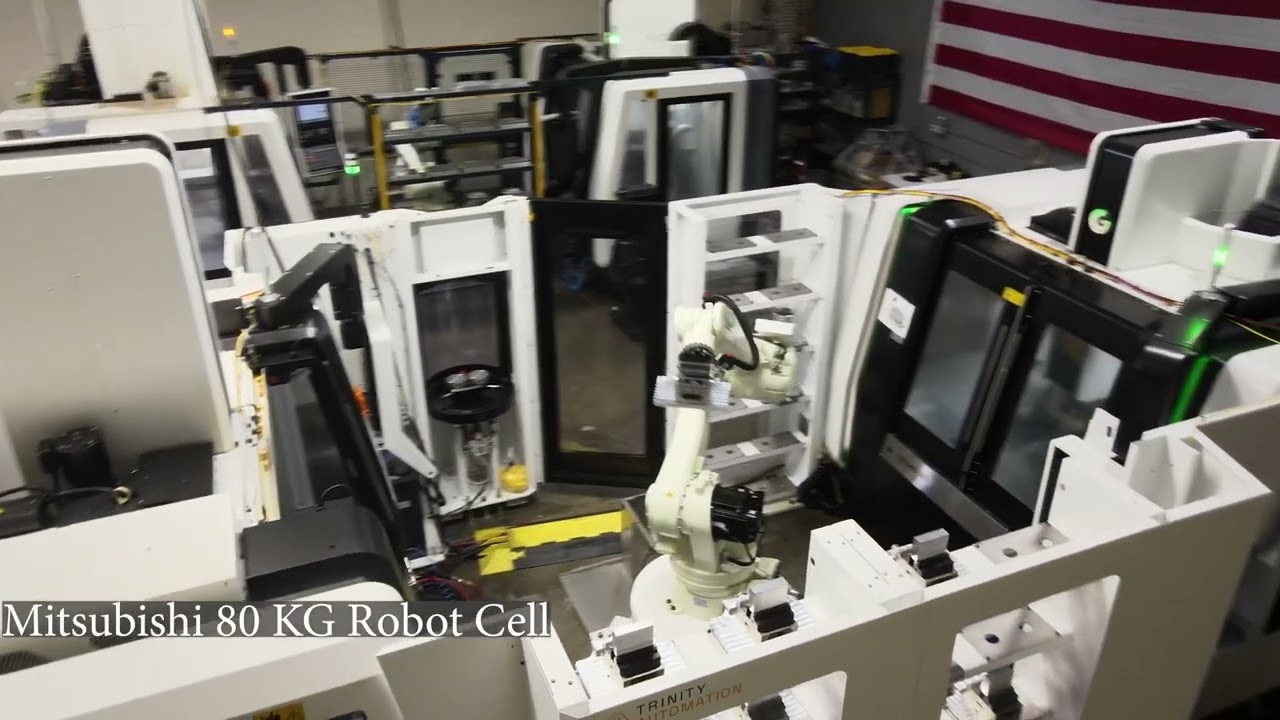
TL Aerotek · Expand customer TL Aerotek running an Expand GEN MILL with Mitsubishi LoadMate Plus robotic machine tending
output vs. manual machine tending
24 hrs
unattended run right after start-up
1 wk
to complete a full month's quota
15 min
to load 10 blanks, then walk away
“Both companies give me what I need: super support, performance, and reliability.”
Tai Le · Owner, TL Aerotek
Source: Mitsubishi Electric Automation customer case study & ASSEMBLY magazine (Feb 2026). Results are TL Aerotek's own; outcomes vary by part, material, and process.
UVM nano-precision · Autonomous machining · 5-axis · Lights-out
Shibaura Machine
Formerly Toshiba Machine — a global leader in ultra-precision and large-format machine tools for over 70 years. The featured platform is the UVM Series: a nano-precision machining center built on a 60,000 min⁻¹ aerostatic spindle and a closed-loop vision system — UVM on DX — that lets the machine measure, compensate, and verify itself unattended. That's nano-precision, running lights-out.
shibaura-machine.com ↗
Shibaura UVM — nano-precision machining
Shibaura Machine · UVM series
Five models · nanometer resolution
Surfaces that go straight to use.
A 60,000 min⁻¹ aerostatic spindle running on compressed air rather than ball bearings, linear-motor axes at 0.01 μm programming resolution, and cooling cast into the machine structure. Published results include a bevel gear forging die cut directly in 90 HRA cemented carbide at 17 nm Ra, mirror-finished moulds at 4–5 nm Ra, and an LED headlamp lens mould where polishing hours dropped by 90 percent.
60,000 min⁻¹4–5 nm Ra90 HRA carbide, directPolishing −90%
Measuring itself while it runsFormEye · ShapeEye · UVM-TSA

At this scale a tool you cannot see is the variable that ruins the part. The UVM measures its own cutter contour during rotation, checks spindle displacement, and if it detects dynamic run-out it re-clamps the tool and tries again rather than cutting the error into the workpiece. That is what makes nano-precision compatible with running unattended.

FormEye
Tool contour
imaged at speed, from φ0.05 mm
ShapeEye
Workpiece form
geometry a probe cannot reach
UVM-TSA
Tool & spindle
length, diameter, displacement
Run-out retry
Automatic
re-clamps the tool when detected
The UVM series, in full → Shibaura Machine ↗
Production bandsawing · Cutoff to near-net · Automated material handling · Lights-out
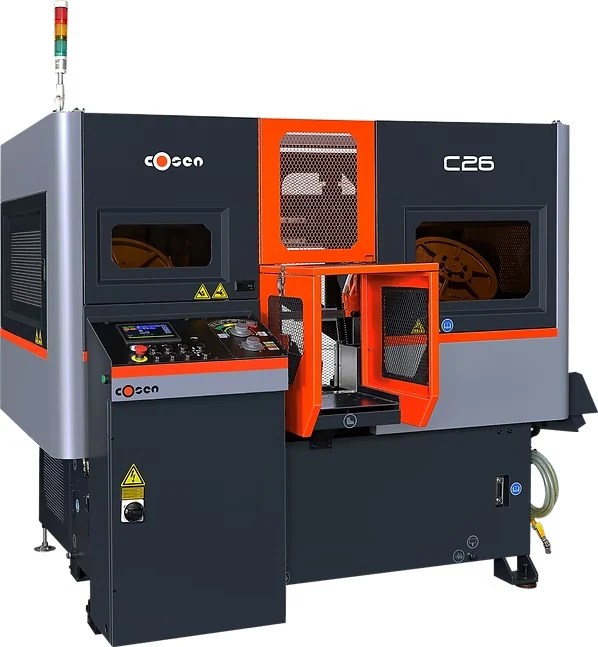
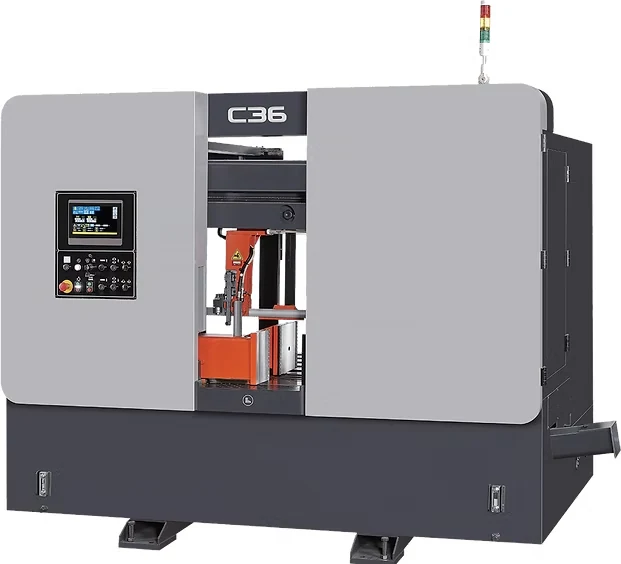
COSENSAWS
Every precision part starts at the saw. As your Cosen distributor, LOMA supplies the first operation too — production bandsawing from raw stock to near-net blanks. Horizontal dual-column, scissor, miter, vertical, and circular cold saws, backed by Q-Cut intelligent control and full material-handling automation — so cutoff runs unattended and the whole cell, from bar to finished part, comes from one partner.
10″–79″
Cutting capacity across the line
Dual-column
Straight, square cuts under heavy production
Q-Cut
Intelligent blade & feed control with cut optimization
Lights-out
Automated bar feed, indexing & material handling
Featured saws
The Cosen range
See the full Cosen range ↗
The lights-out advantage
Every machine we supply is selected for its lights-out capability.

We don't sell machines by catalog. Every machine recommendation starts with one question: will this platform run reliably, unattended, overnight — producing conforming parts when nobody is watching? That question drives every specification we recommend and every builder relationship we've built.
Robotic automation cells — unattended overnight production
Mill-turn centers — done-in-one, zero re-fixturing, zero overnight error
Swiss-type precision — sub-micron accuracy on slender components
Twin-turret twin-spindle — simultaneous front and back machining
5-axis VMC with integrated turning — one setup, complete parts
Compact automation cells — robot-loaded, gauge-verified, lights-out
Machine builders

The builders behind
every machine we place.

LOMA represents a curated group of the world’s leading machine builders — chosen for precision, productivity, and lights-out capability. Here’s who builds what, and the heritage behind it.

Expand Machinery
Chatsworth, California · est. 1985 · Hasegawa import partner
Expand Machinery

Founded in 1985, Expand Machinery builds the GEN TURN Swiss and turn-mill lathes and the GEN MILL machining centers — engineered for the highest value and productivity in accessible precision. Expand is also the North American import partner for Hasegawa Machine Works of Japan, bringing the Made-in-Japan flagship models to the U.S. market. A proud partner of the Arrow McLaren IndyCar team.

Builds: GEN TURN · GEN MILL
Hasegawa Machine Works factory in Japan
Hasegawa Machine Works
Imported by Expand · Saitama, Japan · the leading edge in small machines

The Made-in-Japan models Expand imports — the GEN TURN C24 G, C52 MYS, CW52 MY and CW52MY GII, and the GEN MILL PM320 — are built by Hasegawa Machine Works. Its credo, “the leading edge in small machines,” reflects a singular focus on compact, high-accuracy turn-mill centers: in-house-manufactured spindles and milling turrets, symmetrical thermally-stable construction, and a rigid horizontal bed — the pedigree behind Hasegawa repeatability, shift after shift.

Shibaura Machine precision machining center
Numazu, Japan · est. 1938 · formerly Toshiba Machine
Shibaura Machine

Shibaura Machine — a machine-tool builder since 1938, and known as Toshiba Machine until 2020 — has pioneered ultra-precision machining since developing aerostatic-bearing spindles in 1977. Its UVM nano-precision centers hold sub-micron accuracy and mirror finishes for optical molds, semiconductor components, and the most demanding surface work, with spindle speeds to 60,000 rpm and integrated thermal-displacement control.

Builds: Shibaura UVM
Cosen band saw
Hsinchu, Taiwan · est. 1976 · 50 years
Cosen Saws

Founded in 1976 and marking 50 years, Cosen is one of the world’s largest band-saw manufacturers — 140 models from 8″ to 80″, more than 82,000 saws sold across 80+ countries, and repeatedly rated the No. 1 sawing brand in North America. Cosen’s dual-column, scissor, and CNC automatic saws bring Q-Cut intelligent control and lights-out material handling to the front of the cell, supported from Charlotte, NC.

The problem

Three vendors. Three phone calls.
Nobody accountable.

Most shops juggle a machine tool dealer, a cutting tool distributor, and a CAM consultant — none of whom talk to each other. When something goes wrong, nobody owns the outcome.

Machine dealer
Sells iron. That's it.
No tooling knowledge. No engineers. Support ends the day the machine is commissioned. You figure out the rest.
Tool distributor
Ships carbide. No more.
Can't spec a machine. No CAM support. Recommends tools without knowing your machine, fixture strategy, or tolerances.
CAM consultant
Programs without context.
Writes code but has no tooling or machine expertise. No continuity. You start over every project.
The result
Three invoices. Zero ownership.
When throughput falls or quality misses, everyone points elsewhere. The shop owner is left holding all three problems.
The solution

One partner. One call.
Everything your shop needs.

LOMA brings CNC machinery, cutting tools, and application engineering together under one roof — with engineers who know how all three work together.

"We don't just sell the machine.
We make it produce."

CNC Machinery & Automation

Capital equipment selected, supplied, installed, and commissioned by our team. Not the most expensive machine — the right one for your application.

Machining centers — 3-axis through 5-axis
Turning centers & multi-tasking
Robot cells & automation systems
EDM & grinding equipment
Workholding systems

Cutting Tools & MRO Supply

Proprietary NSHP carbide tooling with manufacturer-verified parameters — plus hundreds of brands as one solution. AI-powered recommendations and predictive reorder.

NSHP Exclusive end mills, drills & inserts
Hundreds of brands, one solution
Predictive reorder engine
Mastercam / Fusion 360 parameter export
Tooling & MRO at nsitools.com ↗

Application Engineering & Programming

Our engineers develop the process, write the programs, and optimize parameters — so you hit cycle time targets from day one, not month three. And they stay involved after the sale. Processes drift, materials change, new work comes in the door — our application engineers keep working with you on process improvement and continuous improvement long after the machine is signed off.

CNC programming & CAM (Mastercam, Fusion)
Application & process development
Speeds, feeds & toolpath optimization
On-site setup & operator training
ROI & cycle time analysis
The tooling side of the house

NORTH SHORE INDUSTRIAL TOOL

Ipswich, MA · serving New England & the Northeast

Most machine deals end at the install. Ours is where the work starts. North Shore Industrial Tool is our sister company — a technical cutting-tool and MRO distributor running hundreds of premier lines, application engineering, and managed inventory for aerospace, defense, medical and precision shops across the Northeast.

That means the machine you buy from LOMA arrives with the tooling package already engineered, the workholding chosen for the part rather than the catalogue, and a crib that refills itself instead of generating a panic order at 2pm. Same people, same phone number, one relationship from the quote to the crib.

Cutting tools & toolholding

Hundreds of premier lines plus the proprietary NSHP carbide range — end mills, drills, inserts, and the holders and shrink-fit that keep runout low at the spindle.

What NSIT manages →

Workholding

German-engineered vises, chucks and zero-point systems — including HWR SOLIDStamp form-fit clamping and the INOFlex VL compensating 4-jaw chuck, both built for 5-axis work.

HWR workholding →

Application engineering

Engineers in the cut, not on the phone. Process development, speeds and feeds, and the cycle-time work that gets a new machine to target in weeks rather than quarters.

Application support →

Managed inventory

Vending, bin stock and predictive reorder run as a program — so consumables show up before the line stops, and you stop carrying inventory you do not need.

Inventory management →
Visit nsitools.com → Or call 978-356-2500 — same number for machines and tooling.
How we work

From first conversation
to lights-out production.

01 / Assessment
We visit your shop
At no cost — our engineer assesses your parts, volumes, tolerances, and current workflow. We understand your constraints before recommending anything.
02 / Specification
Right machine. Right tooling.
Not the most expensive option. Machine selection and tooling strategy are developed together — because they depend on each other.
03 / ROI Analysis
You know the payback first
Cycle time improvement, labor savings, and payback period — calculated before you sign anything. You buy certainty, not a brochure.
04 / Installation
We coordinate the install
Installation and commissioning are handled by the machine builder and our local service partners, coordinated by us — first parts run, operators trained. Production doesn't start until we're both confident.
05 / Programming
We write the programs
Full CNC programs in Mastercam, Fusion 360, or SolidCAM — with verified speeds, feeds, and toolpaths for your machine and material.
06 / Ongoing
We stay with you
Factory service from the machine builder plus local service partners for fast on-site response — with tooling replenishment, reorder prediction, and engineering support for the life of the machine. One call to us, not a runaround.
Who we serve

Manufacturing shops
ready to produce more.

Job shops, contract manufacturers, and OEM production facilities across the Northeast — from aerospace and defense to precision medical, semiconductor, and optics manufacturers.

Satellite in orbit — aerospace precision components
Aerospace · Defense · Space & Satellite
Impeller — aerospace turning
Turbine blade — precision 5-axis
Precision aerospace chucks
Aerospace · Defense · Space & Satellite

Aerospace, Defense & Space

Structural components, engine parts, housings, and precision assemblies in titanium, Inconel, and aluminum. Tight tolerances, exotic materials, full traceability — for aerospace, defense, and a growing space and satellite sector demanding the same precision at higher volumes.

AS9100 supply chain 5-axis prismatic Swiss turning Exotic alloys Space & Satellite Traceability
Milling head — medical precision
Precision nut housing — medical
Medical · Surgical · Implants

Medical Device

5-axis and turning applications in titanium, stainless, and cobalt chrome. ISO 13485 supply chain awareness, exceptional surface finish requirements, and lot traceability. From surgical instruments to implantable components — the right machine, right tooling, right process.

ISO 13485 aware Titanium · CoCr Surface finish Implants
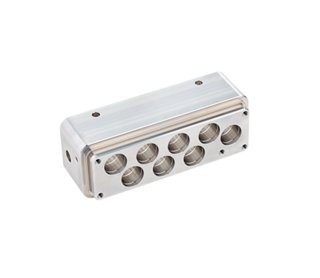
Precision manifold — automotive
Automotive · EV · Tier 1 & 2

Automotive & Tier 2

High-volume machining of aluminum, cast iron, and steel. Automation and robot cells for lights-out production runs. Cycle time and cost-per-part optimization as the primary deliverable — from housings and brackets to transmission and drivetrain components.

High-volume turning Robot automation Lights-out EV drivetrain
Precision chucking components
Job Shops · Contract Mfg · OEM

General Precision Machining

Job shops and contract manufacturers serving multiple verticals. We understand the need for flexibility — our single-source model means faster setup, better decisions, and a permanent partner for tooling, machines, and application support.

Multi-vertical Single-source Application support Fast setup
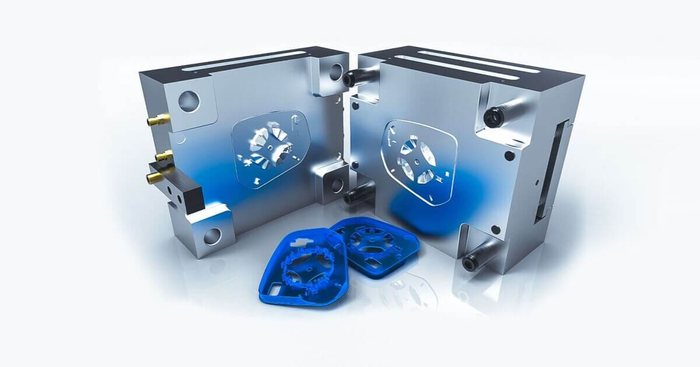
Precision injection mold — die and mold machining
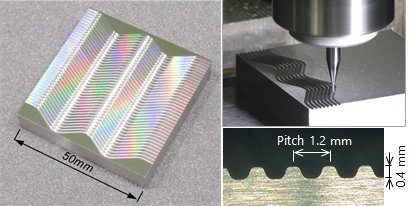
Shibaura UVM — precision optics surface
Diffraction grating · 50mm — UVM 5-axis
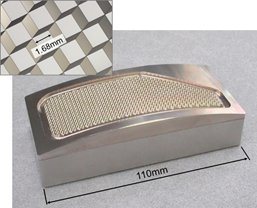
Shibaura UVM — micro-textured optical mold
Micro-lens array mold · 110mm — 10nm Ra
Die & Mold · Precision Optics · Micro-Machining

Mold, Die & Precision Optics

One of the most demanding applications in precision manufacturing — and a core focus of the Shibaura UVM platform. Die and mold shops demand sub-micron surface accuracy, mirror-finish cavity work, and the ability to cut complex 3D freeform geometries without secondary hand-polishing. Optical applications push further still: diffraction gratings, micro-lens arrays, and freeform optics require 10nm Ra surface finish and nanometer-level positioning accuracy only achievable with aerostatic bearing spindles.

Injection mold Die casting mold Freeform optics Diffraction grating Shibaura UVM 10nm Ra Sub-micron
SEMI SEMICONDUCTOR · ELECTRONICS · PHOTONICS
Semiconductor · Electronics · Photonics

Semiconductor & Electronics

Semiconductor equipment and electronics manufacturing demand the most exacting machining tolerances in any industry — wafer handling components, vacuum chamber parts, heat exchanger plates, and photonic device housings all require nanometer-level surface integrity and sub-micron form accuracy. The Shibaura UVM platform with aerostatic bearing spindle and linear motor axes is purpose-built for this class of work, producing chip packaging fixtures, sensor housings, and precision lens mounts directly from program — no hand-lapping required.

Wafer handling Vacuum chambers Photonic devices Sensor housings Shibaura UVM Sub-micron form Lens mounts
Our story

Built by industry.
Built for American manufacturing.

Lights Out Machinery & Automation was founded by experienced industry executives who saw the same problem everywhere they looked: American manufacturers were buying world-class machines and running them with world-class tooling — but without the application expertise to make them perform at their potential.

The gap wasn't in the equipment. It wasn't in the cutting tools. It was in the space between them — the process knowledge, the programming expertise, the speeds and feeds optimization that turns a machine investment into a competitive advantage. That space was occupied by nobody.

Machine tool dealers sold iron and moved on. Cutting tool distributors shipped product without understanding the machines it ran in. CAM consultants wrote programs without accountability for tool life or cycle time. And the shop owner stood in the middle, managing three separate relationships that never talked to each other.

"We didn't build LOMA to be another distributor. We built it to be the partner we wished existed when we were on the shop floor."

LOMA was built to close that gap — permanently. By combining capital equipment supply, precision cutting tools, and full application engineering under one roof, we give American manufacturers the single-source technical partnership that the industry's growth demands.

The American manufacturing resurgence is real. Reshoring is accelerating. Defense spending is rising. Aerospace production is expanding. The shops positioned to capture that growth are the ones with the right machines, the right tooling, and the right engineering support — all working together. That's what LOMA delivers.

LO
Rooted in Massachusetts. Built on decades of combined experience in precision machining, capital equipment, and industrial supply — serving precision manufacturers across the Northeast, from job shops to OEM production floors.
Our mission
To be the partner that American manufacturers deserve — supplying the machines, the tooling, and the engineering expertise to compete and win at the highest level.
Customer success is our success
We measure our performance by your results — not by units shipped. If your shop isn't hitting cycle times, reducing scrap, and running more efficiently, we haven't done our job.
High integrity — we do what we say
We make commitments we can keep and keep the commitments we make. If we say we'll be on your floor Tuesday morning, we're on your floor Tuesday morning. No excuses. No surprises.
Technical excellence over sales pressure
We won't recommend a machine we can't justify with ROI analysis. We won't recommend a tool we don't believe in. Our reputation is built on the quality of our recommendations — not the volume of our transactions.
We stay after the sale
Our relationship with a customer begins at installation and never ends. We're there for cycle time optimization, process changes, new jobs, and new challenges — for the life of the equipment.
🇺🇸
Committed to American manufacturing
We believe in the resurgence of domestic manufacturing and we're building LOMA to accelerate it. Precision machining is a strategic national asset. Helping American shops run better is not just a business — it's a mission.
Single source — fully accountable
One partner for machines, tooling, and engineering means one point of accountability. When something needs attention, there's no finger-pointing between vendors. One call. One relationship. One outcome.
Our family of brands

One partnership.
Machines, tooling & engineering.

LOMA brings the machines and the application engineering. Our sister company, North Shore Industrial Tool, brings the cutting tools and MRO supply. One conversation, one contact, one solution.

Cutting tools & MRO · Sister company
North Shore Industrial Tool

The Northeast's trusted source for carbide cutting tools, NSHP Exclusive tooling, and industrial MRO supply.

NSHP Exclusive carbide end mills, drills, inserts
Hundreds of brands, one solution
MRO consumables and safety supply
Predictive reorder engine
CNC machinery · Launching
Lights Out Machine Tools

CNC machining centers, turning centers, 5-axis machines, and complete automation cells — supplied, installed, and supported by our team from day one.

Machining centers — VMC, HMC, 5-axis
Turning centers & multi-tasking
Robot cells & automation systems
EDM & grinding
Workholding & fixture systems
Application engineering · Launching
Lights Out Engineering

Application engineers and CNC programrs who develop your process, optimize your parameters, and make your machines produce from day one.

CNC programming & CAM support
Application & process development
Speeds, feeds & toolpath optimization
On-site setup & operator training
Cycle time & ROI analysis
Application engineering

Send us the part.
We’ll call you back the same day.

Most machine enquiries start with a spec sheet and a price. Ours start with your part. Send a print, a model, or a photo of the job that is costing you money — and we will call you back the same day to talk through how to make it.

Depending on what the part needs, it gets looked at by our team, the builder’s application engineers, or both together. On a difficult job that means the people who designed the machine are looking at your geometry, not a salesperson forwarding a PDF.

Step 01
You send the job
A PDF print, a STEP file, or a photo and a description. Enough to see the geometry, the material and the tolerance that matters.
Step 02
The right people review it
Our team, Expand’s application engineers, or a combination — whoever the application actually calls for.
Step 03
We call you back the same day
A conversation about the part: which machine suits it, how it would be held, what the tooling looks like, and what we would want to know before quoting.
Step 04
A sample part, where it is warranted
Cutting a sample is decided case by case, as it is across the industry. If your program justifies it, we will talk about proving it on the machine.
What makes this worth your time
More than one set of eyes. Hard parts get reviewed by our people and the builder’s engineers together, rather than by whoever picked up the phone.
Machine and tooling from one source. Cycle time is a tooling problem as often as a machine problem — we work both sides of it.
The engineer stays after the sale. Our application engineers keep working with you on process and continuous improvement once the machine is running — not just through the install.
Your drawings stay yours. We will sign your NDA before you send anything — just ask.
↩ Same-day call back 🔒 NDA on request — before you send ◉ Northeast and beyond ☎ 978-356-2500
Send a part for review
Same-day call back

PDF, STEP, DXF, DWG or an image, up to ~10 MB. Zip several files together, or email larger models to cburns@lightsoutma.com. Need an NDA in place first? Say so below and send nothing until it is signed.
Where these machines go

Different industries, different reasons the part is hard.

Aerospace and space are low volume and high consequence. Medical is slender and tight-toleranced in material you cannot afford to scrap. Production turning is decided by cost per piece. The machine that suits one rarely suits all three — these pages work through why.

Common questions

Automation, cycle time and getting the downtime back.

The questions we get asked most about running unattended, cutting cycle time and keeping spindles turning. If yours isn’t here, call 978-356-2500.

What does it actually take to run a machine lights out?
Four things have to be true. The part has to get in and out without a person — a bar feeder for bar work, a loader or robot for chucked work. Chips, coolant and thermal drift have to be managed for the length of the run. Something has to notice a broken or worn tool before it makes four hundred bad parts. And there has to be enough tooling in the changer to reach the end of the program. Get one wrong and you are not running lights out, you are gambling overnight. We walk through all four on our lights-out machining page.
Do I need a robot, or is a bar feeder enough?
For bar work, a bar feeder and a parts catcher often cover it, and every lathe we supply takes one. You need part handling — a robot or a loader — when the work is chucked, when there is a second operation, or when the blank is not made from bar. The honest answer depends on the part, and it is worth deciding before you buy rather than after.
What is the difference between a collaborative robot and a built-in loader?
A collaborative robot sits beside the machine and can be moved between machines or re-tasked as jobs change — flexible, and the right answer for high-mix work. A built-in loader is part of the machine: the CW52MY GII carries a three-axis gantry overhead reaching both spindles with a 3 kg payload, and the C24 G has a gantry loader with a twelve-station stacking magazine. Built-in costs no floor space and needs no cell fencing, but it does what it was designed to do rather than whatever you point it at.
Can automation be added to a machine I already own?
Usually, yes. Bar feeders, parts catchers, robot cells and pallet systems get added to existing machines regularly. What decides feasibility is control integration, whether the machine can signal cycle complete and accept a start command, guarding, and floor space. Send us the machine model and the part and we will tell you what it would take.
How much turret index time am I actually losing?
A turret indexes in roughly one to three seconds between tools — the machines in our range run 0.8 to 3.2 seconds tool-to-tool. Multiply that by tool changes per part, then by annual volume. On a short-cycle, high-volume job it adds up to real spindle hours, which is exactly why gang-tooled lathes exist: every tool sits on a slide that is already moving, so the next tool arrives as the slide travels and there is no index at all.
What is the fastest way to cut cycle time without buying a machine?
Usually tooling and process before iron. Better substrate and coating, correct speeds and feeds for the actual material condition, fewer tool changes, and eliminating a second operation are all cheaper than a new spindle. That is why we work both sides — through North Shore Industrial Tool we supply the cutting tools and application engineering as well as the machine, so the recommendation is not automatically "buy something".
Why do second operations cost more than they look?
Because the cost is not the cycle. It is the handling, the extra setup, the fixture, the WIP sitting between machines, the risk of scrapping a part that is already half finished, and a second chance to lose datum. Machines that finish a part complete — Swiss with back working, twin-spindle turn-mill, 5-axis milling — are usually justified on that rather than on cycle time alone.
What causes unplanned downtime, and what actually reduces it?
In practice: tool failure nobody caught, chip and coolant problems, setups running long, and waiting on tooling that was not in the crib. Tool life management and probing address the first, conveyors and coolant capacity the second, quick-change tooling and workholding the third, and a managed inventory program the fourth. Only one of those four is a machine purchase.
Does running unattended compromise accuracy?
Not if the machine can verify itself. The Shibaura UVM images its own cutter contour while it is spinning, checks spindle displacement, and re-clamps the tool when it detects dynamic run-out rather than cutting the error into the workpiece. Spindle chillers and thermal stabilising systems hold position across a long run. Accuracy and unattended running meet at self-measurement — a machine that cannot check its own condition is the one you should not leave alone.
Can high-mix, low-volume work be automated, or only long runs?
Both, but differently. Long runs justify dedicated handling — a bar feeder or built-in loader running one part for a shift. High-mix work is better served by flexible automation: a collaborative robot that can be re-taught, quick-change workholding, and machines that finish parts complete so there is less to schedule. The mistake is buying long-run automation for a high-mix shop and then fighting the changeover.
What should I work out before automating?
How many unattended hours you would actually gain, what the machine does when something goes wrong, who reacts and how quickly, and what happens to the operator's time once it is freed up. Automation that runs four hours unattended and then needs two hours of morning cleanup has not gained you six hours. That arithmetic is worth doing on your own numbers before anyone quotes you.
What happens after the machine is installed?
Our application engineers stay involved. Run-off and operator training are the start, not the finish — processes drift, materials change, tool life shifts, and new work comes in the door that nobody planned for when the machine was quoted. We keep working with you on process improvement and continuous improvement: revisiting speeds and feeds, cutting setups out, extending tool life, and taking cycle time out of jobs you are already running. Because we supply the cutting tools and the machine, that work does not stop at the boundary between two suppliers.
What kind of parts do these machines make?
Aerospace impellers and bladed geometry, turbine and energy components, space and defense hardware, medical and orthopedic parts such as bone screws and instrument components, and high-volume precision turned parts. Different problems: aerospace and space are low volume and high consequence, medical is slender and tight-toleranced in expensive material, and production turning is decided by cost per piece.
Free engineering assessment

Ready to run
lights out?

Send us the part. We'll tell you how to make it — faster, tighter, and lights-out. Every machine is sold on the application and backed by the builder's factory engineers.

Machine
A recommendation matched to your part, materials, and volumes.
Tooling
A complete cutting-tool and workholding spec.
Process
An application and CNC programming approach to get it running.
The numbers
Cycle-time and cost-per-part guidance, where the part allows.

Optional. PDF, STEP, DXF, DWG, or an image — up to ~10 MB. Zip multiple files, or just email larger models to info@lightsoutma.com.
Send your print → an application engineer reviews it → you get a written recommendation. No obligation.